Turnkey Complete Cleanrooms Manufacturer: Streamlining Your Path to a Certified Controlled Environment
2026-11-16
Building a controlled environment that meets stringent certification standards can feel like navigating a maze of regulations, design choices, and vendor coordination. One misstep—whether in airflow design, material selection, or documentation—can delay your project by months and inflate costs unexpectedly. That’s why more companies are turning to a single partner who can handle every phase: from initial concept and modular construction to final validation and handover. GENO Pharmatech specializes in turnkey cleanroom solutions that eliminate the guesswork, letting you focus on your core operations instead of managing a dozen subcontractors. In this post, we’ll break down what a true turnkey approach actually includes, the hidden pitfalls it helps you avoid, and how it streamlines your path to a fully certified controlled environment.
From Blueprint to Certification: One Team, Zero Guesswork
Every project starts as a rough sketch, a set of dimensions, a handful of ideas scribbled on paper. From there, the path to a finished building can feel like a maze of approvals, inspections, and last-minute changes. We bring that journey under one roof, so you never have to chase down a dozen different contractors or wonder if the engineer actually saw the latest revision. Our team moves with you from the first line on the blueprint to the final sign-off, keeping every detail aligned and every deadline in sight.
The old way meant juggling architects, structural engineers, permit runners, and field crews, each with their own schedule and their own version of the truth. We changed that. Instead of passing drawings back and forth and hoping for the best, you get a single point of contact who knows the project as well as you do. We review the plans together, flag potential issues before they become expensive surprises, and handle the paperwork, the code checks, and the on-site coordination. No guesswork, no phone tag, no waiting weeks for a simple answer.
When the final certification lands in your hand, you should feel confident that the structure matches the vision you started with. That confidence comes from a process built on transparency and shared responsibility. We track every change order, every inspection note, and every material substitution in one place, so nothing slips through the cracks. From blueprint to certification, it is one team, one plan, zero guesswork.
Cleanroom Design That Fits Your Process, Not the Other Way Around
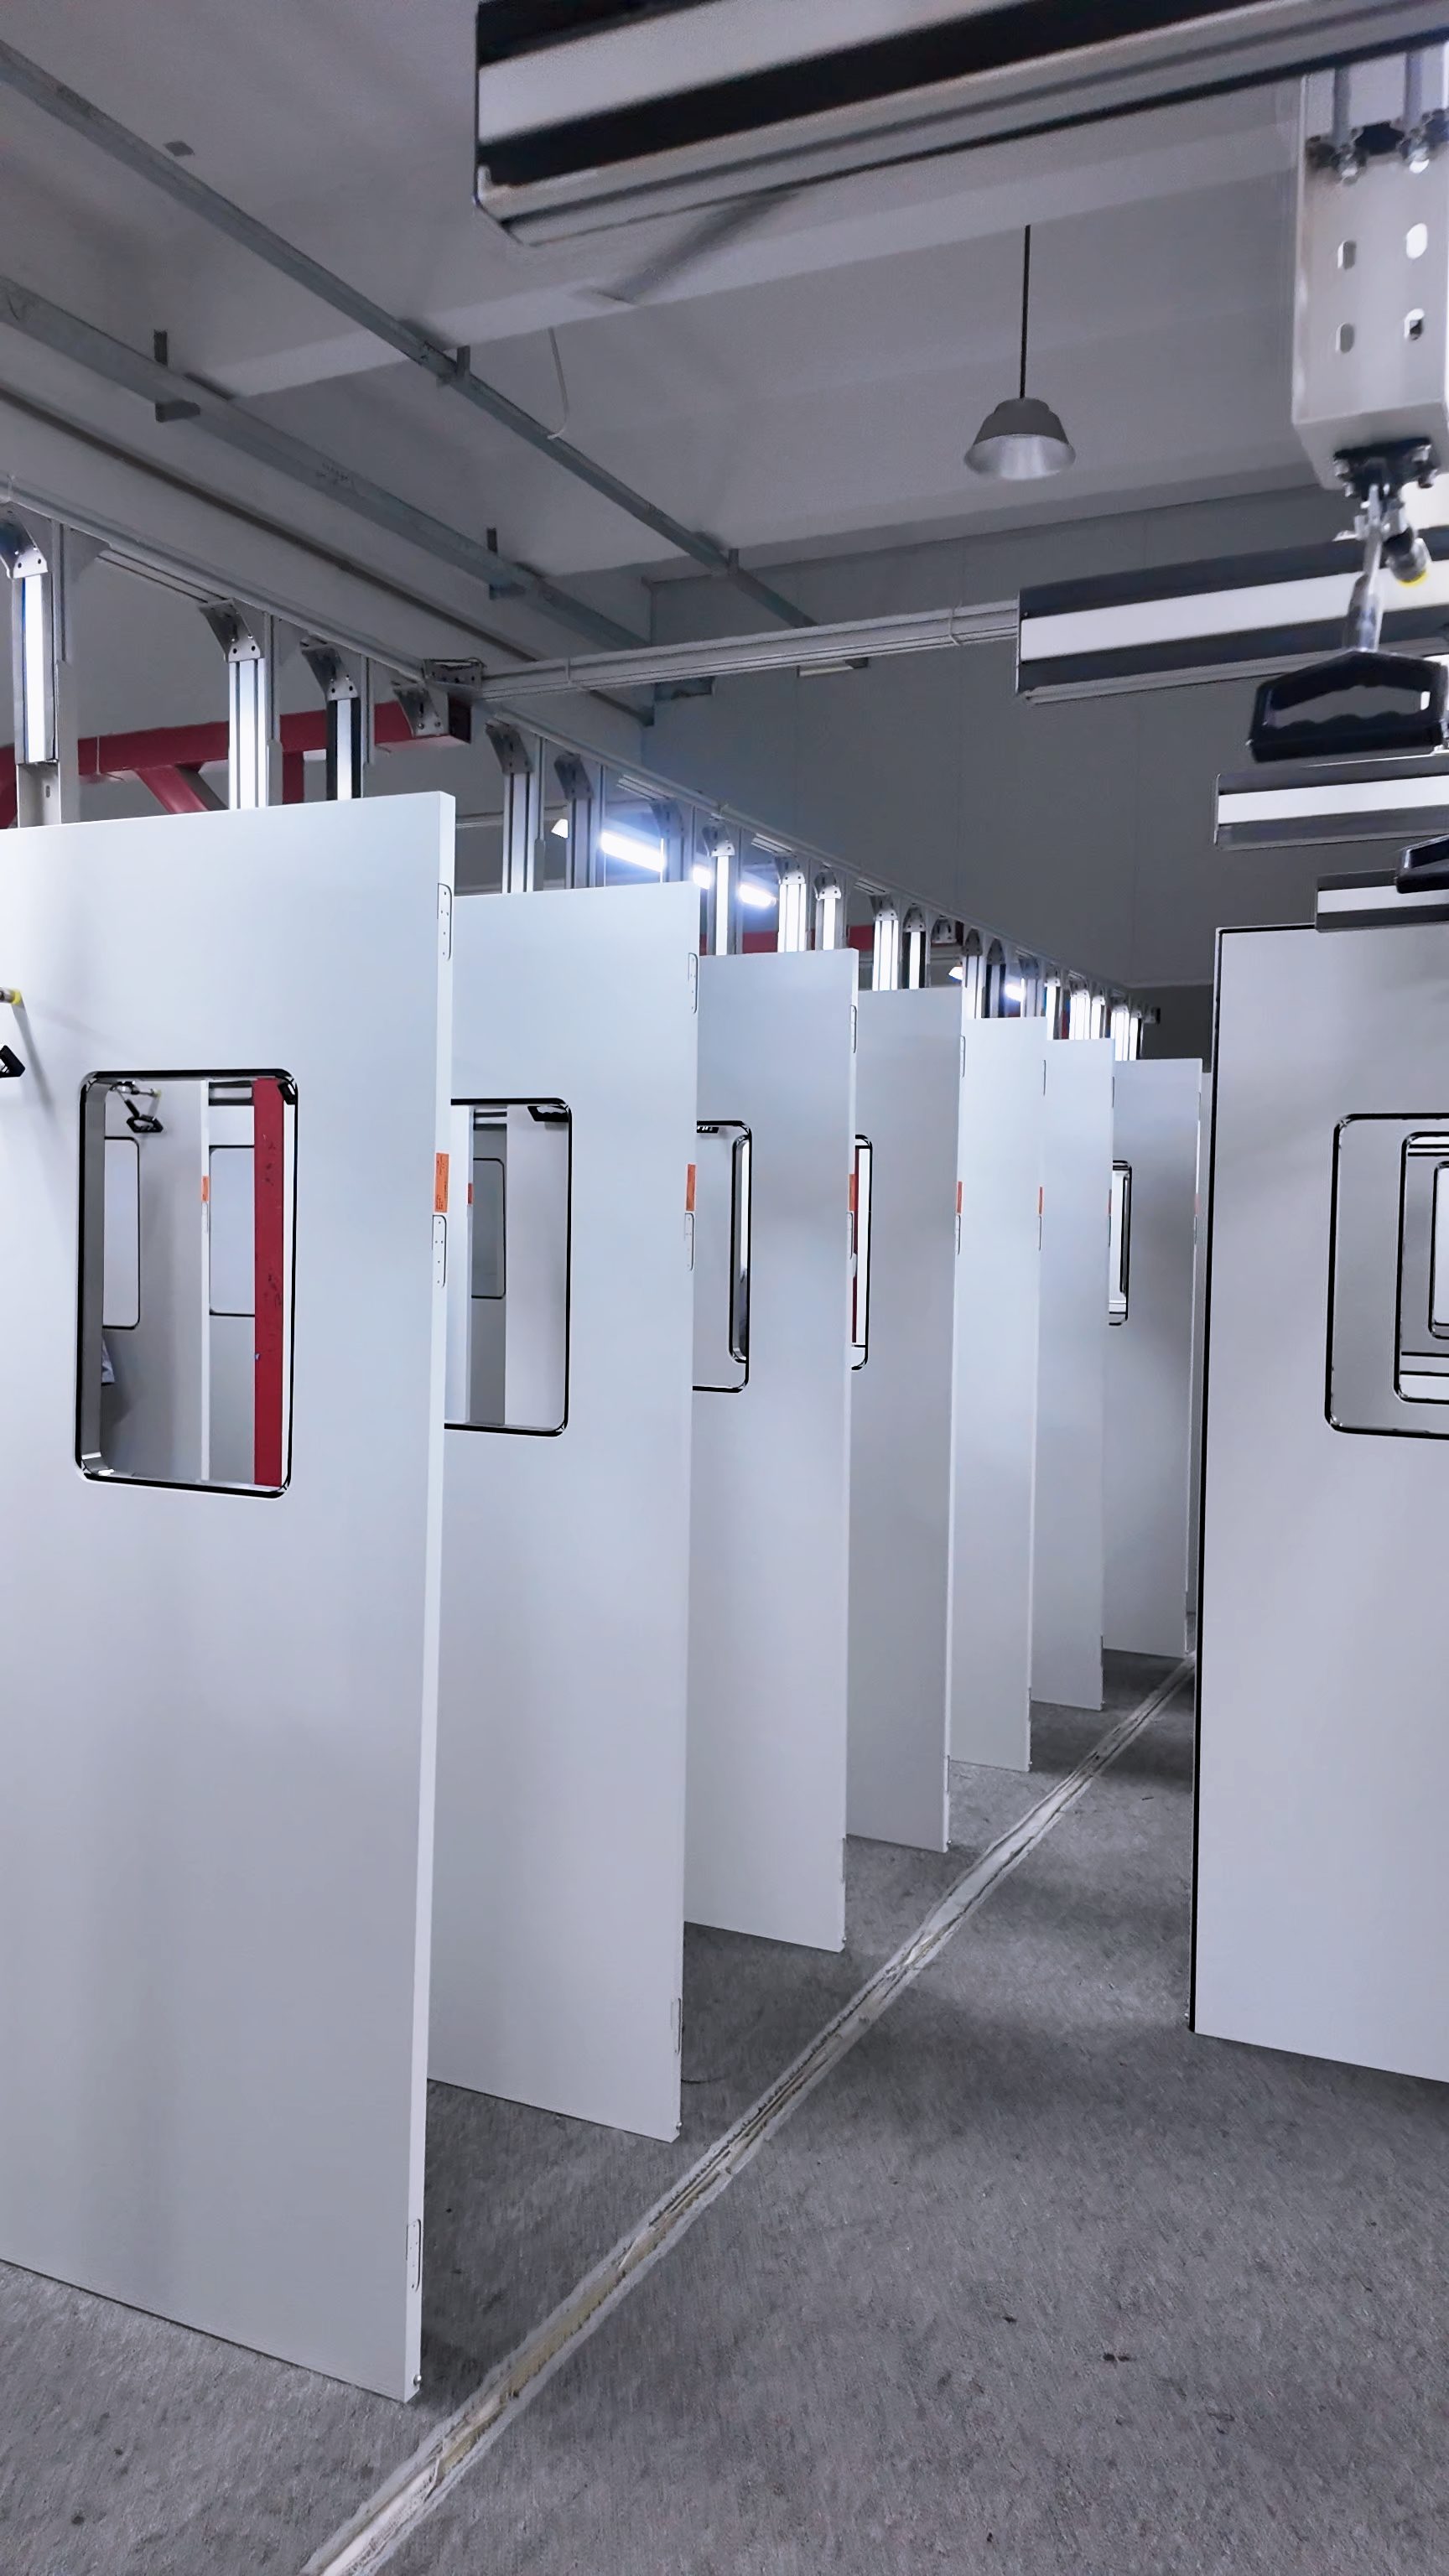
Most cleanroom projects start with a rigid set of specifications, forcing your manufacturing workflow to bend around the room. We take the opposite approach. By mapping every step of your process first, we design the cleanroom around how materials move, where operators stand, and what contamination risks actually exist in each zone. The result is a facility that feels less like a constraint and more like a natural extension of your production line.
That means questioning defaults: Do you really need ISO 5 across the entire floor, or just at the filling station? Can air returns be placed to work with your existing equipment layout instead of against it? By tailoring airflow patterns, filtration placement, and pass-through locations to the realities of your process, we eliminate wasted space and reduce the number of times a technician has to walk from one end of the room to the other.
The payoff shows up in your daily operations. Fewer gowning steps, shorter transfer distances, and cleaner handoffs between stages. You get a room that supports your throughput targets without forcing you to redesign how you work. And if your process changes down the line, the cleanroom is built to adapt, not to dictate.
Modular Construction That Cuts Build Time Without Cutting Corners
Most people assume faster construction means weaker results, but with modular building that trade-off simply doesn't exist. The speed advantage comes from parallel workflows: while the foundation is being poured on site, wall panels, floor cassettes, and roof trusses are already being fabricated in a controlled factory environment. Weather delays, material shortages, and scheduling conflicts that typically stretch a project for months are engineered out of the process from day one.
What often surprises first-time clients is how rigorous the quality control actually is. Because each module is built indoors with precise jigs and repetitive assembly steps, every connection is checked against tight tolerances before it ever leaves the factory. Structural engineers review the same load paths, the same fire-rated assemblies, and the same insulation details they would for a conventional build—except the inspection happens under a roof, not in the mud. The result is a structure that often exceeds code requirements, not just meets them.
The real test comes months after handover, when owners notice the details: doors that still close perfectly because the frame never twisted, drywall seams that never cracked, and utility bills that stay low because the envelope was sealed in a clean environment. That's the quiet proof that cutting build time doesn't have to mean cutting corners—modular just removes the wasted motion, not the craftsmanship.
Certification-Ready Compliance: ISO, GMP, and Beyond
Achieving certification is rarely a box-ticking exercise. It demands a mindset where quality systems are woven into daily operations rather than bolted on for audit season. For ISO 9001 or 13485, the real work happens long before the auditor arrives: risk-based thinking applied to supplier selection, document control that actually reflects how teams work, and corrective actions that treat root cause analysis as a learning loop instead of a blame game. The goal is not just to pass, but to make the standard invisible—embedded so thoroughly that compliance becomes a byproduct of good practice.
GMP adds another layer, especially for manufacturers dealing with consumables or medical devices. The focus shifts to environmental monitoring, contamination control, and batch traceability that can survive a regulator's scrutiny at 2 a.m. But beyond the written SOPs and cleanroom logs, GMP readiness is about culture: operators who instinctively flag a torn glove or an out-of-spec reading because they understand the downstream risk, not because a checklist told them to. Companies that treat GMP as a living system—regularly challenged, simplified, and retrained—tend to sail through inspections while others scramble to patch gaps.
Then there's the territory beyond ISO and GMP: industry-specific schemes like IATF 16949, AS9100, or sustainability certifications that are quietly becoming prerequisites for global contracts. The smart approach is to build one integrated management system rather than a pile of disconnected certificates. Map overlapping requirements once, align internal audits to cover multiple standards in a single pass, and use the same data for management reviews across all frameworks. This not only reduces duplication but also surfaces hidden synergies—like how a robust change control process under ISO can strengthen GMP validation or vice versa. Certification-ready doesn't mean preparing for each audit separately; it means designing operations so that any auditor, from any scheme, finds the same coherent story of control, improvement, and accountability.
Real-World Performance: Built for Semiconductors, Pharma, and More
When your production line runs on precision, generic benchmarks stop mattering. Our systems are dialed in for the unforgiving demands of semiconductor fabs, pharmaceutical cleanrooms, and other high-stakes environments. Instead of chasing idealized lab numbers, we tune every subsystem—thermal management, vibration damping, and motion control—to hold tolerances when the pressure is on. The result is a platform that doesn't just pass validation; it keeps passing it shift after shift.
What sets this apart is the way we handle the messy realities of real-world workflows. In pharma, that means maintaining sterility while swapping tools mid-batch. In semiconductor packaging, it means absorbing micro-shocks from adjacent equipment without losing alignment. We've spent years collecting failure data from actual deployments, then used it to eliminate the weak points that only show up after thousands of cycles. That's why our uptime numbers come from customer floors, not from a controlled demo cell.
You'll notice the difference in the details. Cable routings that don't snag during high-speed indexing. Seals that shrug off aggressive cleaning agents. Software that recovers gracefully from power dips instead of throwing a fault. These aren't glamorous specs, but they're what keep your yield high and your maintenance team off the emergency line. Build a line around equipment that performs where it counts—on the factory floor, not just in the brochure.
Transparent Costs, No Hidden Change Orders
You get a line-by-line breakdown of every dollar before work begins. Materials, labor, permits, disposal fees — each item is itemized so you can see exactly where your money goes. No vague “miscellaneous” line items that balloon later. If a supplier quotes us a range, we show you the high end up front, not the low end to win the job.
Any change to the original scope — whether it’s moving a wall, swapping a fixture, or addressing unexpected rot behind the drywall — gets a written change order with a fixed price attached. You approve it before we touch anything. We don’t invoice you for “extra time” that mysteriously appears at the end of the month. Surprises happen on remodels, but surprise bills don’t have to.
Most change orders stem from poor planning or rushed measurements. That’s why we spend more time on the front end — photographing, measuring, and asking questions about how you actually use the space. It cuts down on mid-project discoveries. And when a real change is unavoidable, you’ll get a clear option with the cost, the reason, and the timeline before you say yes.
FAQ
Everything from initial layout and HVAC design to walls, flooring, lighting, and certification support. The manufacturer coordinates the entire build so you're not juggling multiple contractors.
By baking compliance into the design from day one. They handle pressure cascade testing, particle counts, and documentation so the final audit isn't a surprise.
Most projects target ISO 7 or ISO 8, but experienced manufacturers can go down to ISO 5 or even cleaner with the right fan filter units and airflow design.
Absolutely. You can choose modular wall panels, pass-throughs, gowning rooms, and finishes that match your process needs rather than accepting a one-size-fits-all shell.
For a typical 500 to 2,000 square foot modular room, expect 8 to 16 weeks from design approval to handover, depending on utilities and certification scheduling.
Yes, you should receive IQ/OQ protocols, HEPA filter test reports, air change rate data, and room certification certificates as part of the closeout package.
Reputable manufacturers offer annual re-certification, filter replacement, and emergency troubleshooting. Some also provide remote monitoring so you can track pressure and particle levels between audits.
Conclusion
A turnkey cleanroom partner should remove friction from the very first conversation, not just at handover. Instead of asking you to adapt your workflow to a pre-set footprint, the design process begins with how your operators move, where your equipment sits, and what particle counts your product can actually tolerate. Modular construction then turns that bespoke layout into a physical space in a fraction of the time of traditional stick-built rooms, using pre-engineered panels and integrated utilities that are assembled on site without welding dust or excessive downtime. One accountable team carries the project from initial sketch through pressure differential testing and final certification, so there is no finger-pointing between architect, contractor, and validator when a deviation appears. This single-source approach means the cleanroom is not just delivered on paper but proven to perform under real operating conditions before you run your first batch.
Compliance is treated as a design input rather than a retrofit checklist. ISO class limits, GMP annex requirements, and industry-specific guidelines are baked into material selection, airflow patterns, and gowning flow from day one. For semiconductor fabs that demand ultra-low particulate levels or pharma suites that need rigorous aseptic protocols, the room's performance is verified through third-party testing, with documentation handed over in a format your quality team can drop straight into an audit. Equally important, the quoted price includes the full scope—structural, mechanical, electrical, controls, and validation support—so there are no surprise change orders after ground is broken. Every line item is visible before you commit, and any necessary adjustment is agreed upon in writing. The result is a controlled environment that meets your process needs, your regulatory obligations, and your budget without hidden contingencies.
Contact Us
Contact Person: Amy Yang
Email: [email protected]
Tel/WhatsApp: 008619330882686
Website: https://www.genopharmatech.com/