Triisopropanolamine Manufacturer Evaluation Checklist for Industrial Buyers
2026-11-18
Most triisopropanolamine suppliers can send a certificate of analysis. Far fewer can explain exactly how they will respond when a bulk order fails incoming QC or a production schedule shifts by a week. That gap is where sourcing risk quietly builds. This checklist is designed for industrial buyers who want to move beyond data sheets and sales calls, evaluating manufacturers on the operational details that determine whether a supply relationship stays stable. Use it to pressure-test any candidate, including HAISEN, before signing off on a new source.
What the Production Floor Can Tell You Before the Audit
Walk through the line an hour before auditors arrive and you'll notice what no binder of procedures ever shows. Operators might be reworking a batch of housings at the far bench, not because the spec changed, but because the torque gun drifted out of calibration two shifts ago. Stacked totes near the curing area often hide the real story: a downstream bottleneck that pushes work-in-process into places it was never meant to sit. The floor rarely lies the way a polished readiness report can. If you listen, it tells you which measurements are being taken with a tired gauge, which labels are being reprinted by hand, and which inspection steps get quietly skipped when the line speed climbs.
Look at what people reach for when they think no one is watching. A handwritten cheat sheet taped inside a cabinet door is not a training failure; it's a signal that the official work instruction doesn't match the actual sequence of operations. Scrap bins placed too far from the press invite shortcuts. A missing shadow board outline for a go/no-go pin means someone is probably using a substitute tool that never made it into the calibration log. These are not minor housekeeping issues. They are evidence of drifting process controls that an audit can turn into findings if nobody corrects them at the source first.
A candid fifteen-minute walk with a shift lead usually yields more than a two-hour document review. Ask what they would fix if they had one free weekend and a small budget. Their answer rarely mentions new software or more training videos. It points to a leaky air line that causes intermittent clamp pressure, a scale that drifts in the afternoon heat, or a label printer that jams on the second shift. Fixing those small physical irritants before the audit closes the gap between what the procedure says and what the floor actually does. That gap is where most findings are born.
Reading Between the Lines of a Certificate of Analysis
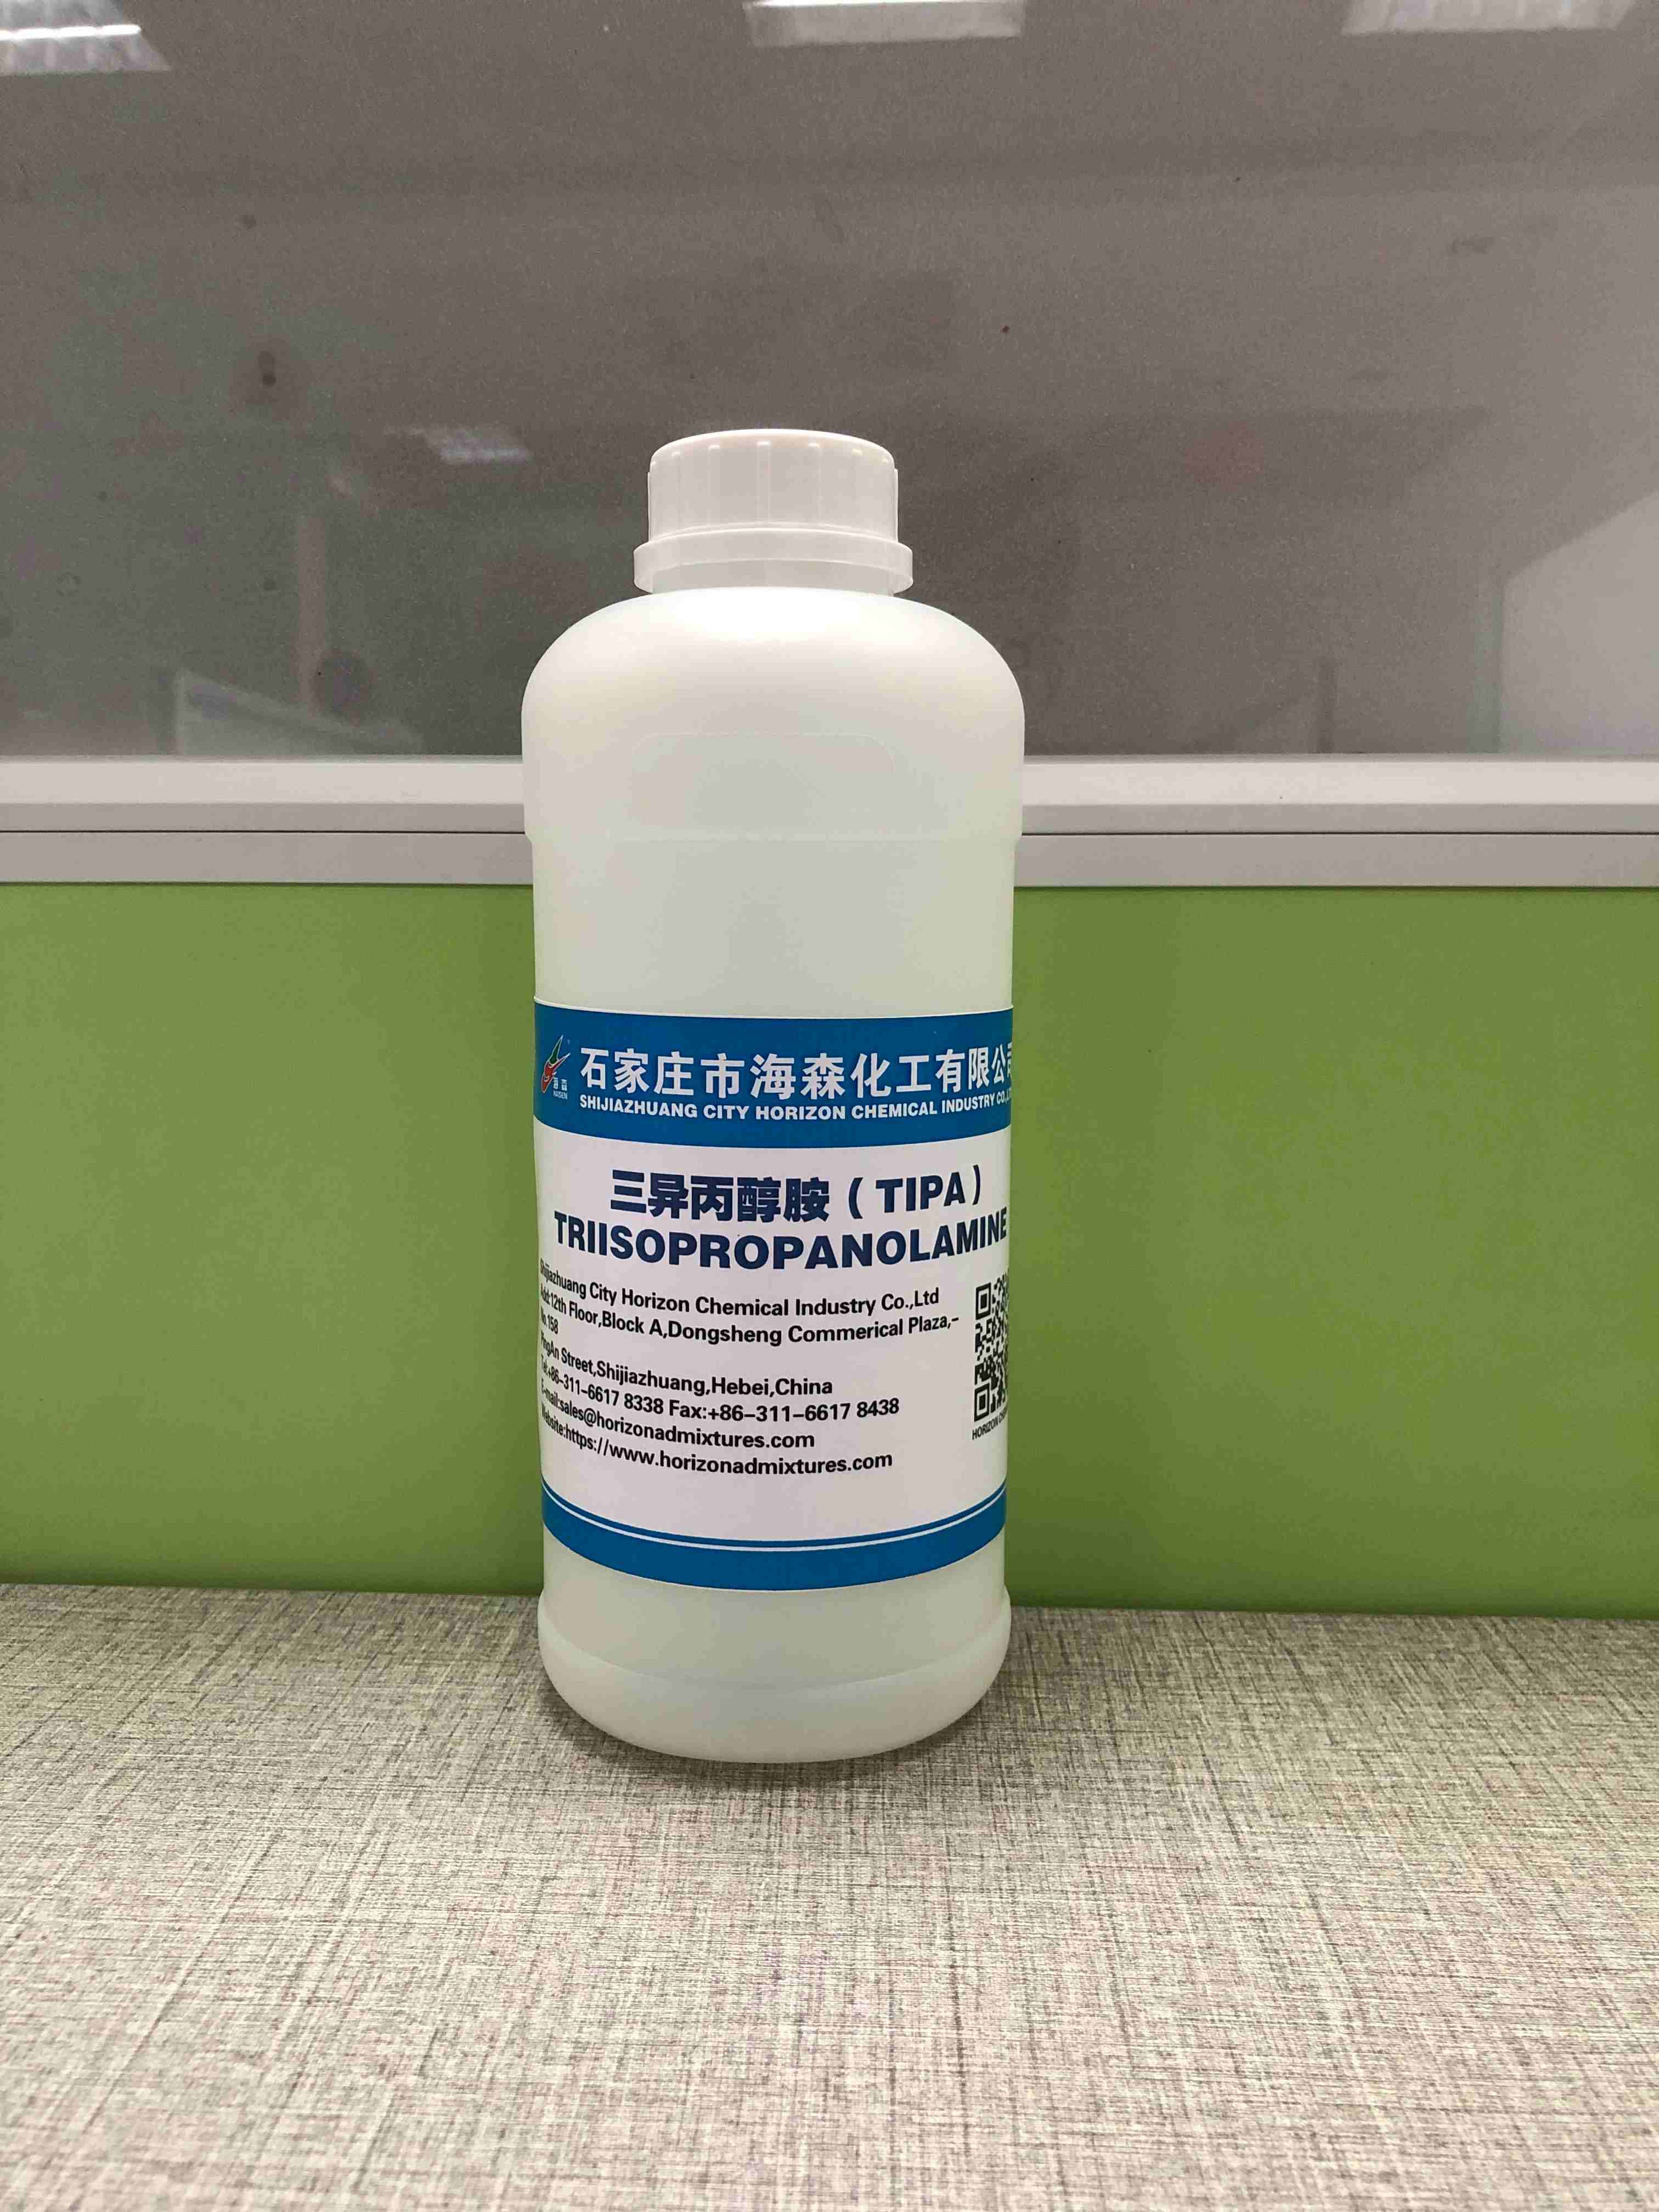
Most people glance at a Certificate of Analysis and simply look for the word "conforms." That habit hides a lot of useful information. The real story often sits in the method column, the way a result is reported, and the distance between the measured value and the stated limit. A value that comfortably clears the limit suggests one kind of process control, while a result that barely passes can point to batch-to-batch drift, even when the paperwork is technically clean.
Missing entries deserve as much attention as the data that is present. If a potential impurity, residual solvent, or microbiological parameter is not listed, it does not automatically mean the material is free of that concern. It may simply mean it was not tested under the supplier's standard scope. In practice, this is where a vague certificate and a genuinely useful one diverge. A well-designed CoA names the method, gives a clear detection or reporting threshold, and avoids hiding behind a blanket statement that offers very little about what was actually measured.
The issue date and the storage conditions printed near the bottom can also change how the certificate should be read. A certificate generated long before shipment may not reflect what happens during transit or extended warehousing. For materials that are sensitive to heat, humidity, or light, the official result is only a snapshot of the product at one moment. Treating the CoA as one part of an incoming material risk assessment, rather than the final word on quality, is usually the more realistic approach in a working lab.
Supply Chain Habits That Keep Your Line Running
Most line stoppages don't start with a dramatic equipment failure. They trickle in from quieter places: a reorder point that was set years ago and never revisited, a supplier lead time that quietly stretched from five days to nine, a receiving dock that accepts everything without checking whether the carton count actually matches the packing slip. These habits slip into daily operations so gradually that nobody notices until the line goes dark for twenty minutes and everyone scrambles to borrow parts from a sister facility.
The teams that keep their lines moving tend to treat inventory accuracy as a living practice rather than an annual audit. They walk the floor with a scanner in hand, correct discrepancies on the spot, and flag any item that shows up damaged or mislabeled before it reaches the point of use. They also build small buffers around the materials that have the most variable lead times, not by hoarding excess stock, but by mapping which suppliers consistently miss promised dates and adjusting order timing accordingly. That kind of granular awareness often matters more than having a sophisticated ERP system.
Another habit worth borrowing is communicating changes in real time rather than waiting for a formal meeting. When a critical component is running low, the best-run lines hear about it during a brief stand-up huddle, not in an email sent after the shift ends. Operators, material handlers, and buyers share the same board or app, updating quantities and expected arrival times as soon as something shifts. This routine removes the three-hour gap between noticing a shortage and doing something about it, which is usually the difference between a smooth afternoon and a pile of unplanned downtime.
Technical Conversations That Separate Order Takers From Problem Solvers
A real problem solver doesn’t wait for a customer to spell out every detail. They listen for what isn’t being said, ask questions that get past the surface, and connect the dots between a complaint and the deeper frustration behind it. Order takers repeat the spec sheet; problem solvers figure out why the spec might not be the right fit at all.
The difference shows up in small moments. When a part doesn’t exist off the shelf, an order taker says “we don’t carry that.” A problem solver says “let’s check what you’re actually trying to accomplish, because two other parts might get you there faster.” That shift from catalog thinking to outcomes thinking is what customers remember long after the invoice is paid.
It’s not about having a bigger brain or more product training. It’s about refusing to hide behind the phrase “that’s just how we do it.” Problem solvers treat every request as a chance to learn the customer’s real constraints, then bend the available options until something actually works. That habit builds trust no scripted pitch can match.
Safety and Handling Support That Shows Up Early
New drivers often discover that the most reassuring safety features aren't the ones that wait for something to go wrong. It's the quiet guidance during ordinary maneuvers—gentle steering adjustments on a wet curve, or a braking nudge when traffic ahead suddenly slows—that builds real confidence. When that support feels present from the first mile rather than as a last-resort intervention, the whole driving experience shifts from cautious to composed.
What makes early handling support stand out is how unobtrusively it works. There's no dramatic warning light or jarring correction, just a subtle, continuous read of the road and the vehicle's behavior. It's the difference between being told you're drifting and simply never feeling the drift in the first place. That proactive character matters most to families and first-time buyers who want a car that feels stable without demanding constant vigilance.
Over time, this kind of early intervention reshapes driver expectations. You begin to trust that the vehicle will smooth over small mistakes, hold the line through an unexpected puddle, or ease you back into your lane before you even realize you've wandered. It's support that doesn't perform for the dashboard—it simply blends into the drive, making safety feel less like a feature and more like a natural part of how the car moves.
Commercial Flexibility Without the Guesswork
Teams rarely grow on a fixed schedule, and a lease should not pretend otherwise. The real advantage shows up when you can shift footprints, add desks, or scale back without renegotiating buried clauses. Most options look flexible on a tour; the difference is how plainly the terms are written so you know exactly what a change will cost before you ask.
That clarity changes the conversation. Instead of running every request through a broker and waiting for approval, managers can make space decisions in an afternoon because the rate card, notice periods, and renewal paths are already visible. The guesswork disappears when the trade-offs are on the table from day one.
What remains is a setup that bends around the business rather than the other way around. You keep the room you need during a seasonal push, trim back during a quiet quarter, and carry the same agreement forward without having to re-open the entire contract. It is adaptability that feels routine, not like a special favor.
FAQ
Look for evidence of batch-level traceability from raw amine sourcing through final blending, and whether they use statistical process control on amine value, moisture, and color rather than relying only on end-product certificates.
Request retained samples from the last three production campaigns and have them independently tested for residual mono/diisopropanolamines, water, and APHA color. Compare variability between lots, not just a single certificate.
Ask about dedicated versus shared storage, lead time under feedstock disruption, and whether they offer regional safety stock with a named inventory replenishment threshold. Consistent answers on minimum order quantities and demurrage experience are often more telling than marketing language.
Low-level secondary amines can affect set time, foaming, or side reactions even when TIPA assay looks high. Ask for a typical chromatogram with identified peaks above 0.05%, not just a percentage.
A complete REACH/SDS package, product registration status in the destination country, and transport classification for TIPA under current regulations. If they cannot clarify whether it is a dangerous good for the chosen shipping route, that is a warning sign.
Check unannounced retained sample test results, housekeeping around amine loading and drumming lines, nitrogen blanketing practice during storage, and how they handle returned or off-spec material. Documentation alone is less useful than watching how operators handle a nonconformance.
Ask whether the manufacturer indexes TIPA pricing to propylene oxide or isopropanolamine feedstock movements, and how often they refresh it. Suppliers that explain formula-based adjustments are easier to forecast than those offering 'special' one-time discounts.
Look for application-specific guidance on handling viscosity at low temperatures, blending with water or other alkanolamines, and compatibility with common formulations. A supplier who can discuss dosing adjustments and field complaints has actual downstream experience.
Conclusion
A plant visit or even a pre-audit conversation about the production floor often reveals more than a polished data sheet. For triisopropanolamine buyers, the way a manufacturer handles raw material staging, moisture control, and batch traceability says a lot about whether the amine will arrive with consistent color, low water content, and predictable reactivity. Instead of accepting a certificate of analysis at face value, experienced purchasers compare the reported impurity profile and test methods against their own downstream tolerances. Small shifts in residual mono- or diisopropanolamine content or unlisted by-products can quietly alter cure rates or emulsion stability, so the numbers between the lines matter as much as the headline assay.
Beyond the lab, supply chain habits keep a production line running: realistic lead times, sensible packaging options, and a clear contingency plan for seasonal logistics all reduce the risk of a stalled order. Technical conversations are another filter. A supplier who asks about your formulation conditions, storage temperature, or blending sequence is more likely to troubleshoot than one who only confirms availability. Early safety and handling support, such as practical unloading guidance, spill containment advice, and accessible documentation, signals that the manufacturer understands triisopropanolamine in real industrial settings. Finally, commercial terms should be transparent, for example, volume flexibility, pricing mechanisms tied to raw material indexes, and credit options, so buyers can plan without guesswork.
Contact Us
Contact Person: Sam Lee
Email: [email protected]
Tel/WhatsApp: 86-311-6617 8338
Website: https://www.horizonadmixtures.com/