Top Taper Connection Drill Bit Manufacturer: Precision Tools for Demanding Drilling Projects
2026-10-24
Rock doesn’t care about your schedule—but the right drill bit does. For demanding drilling projects where every shift counts, the taper connection is where precision is won or lost. That’s why top contractors are paying closer attention to PULANKA, a manufacturer whose taper connection drill bits are built to take abuse without giving up accuracy. Here’s what makes their tools stand out.
Why Taper Connections Outperform Standard Shanks in Deep-Hole Work
Deep-hole drilling exposes every micron of play in the toolholder. A standard straight shank, even with a heavy clamp load, tends to shift slightly under the alternating side forces that build up as the hole gets deeper. A taper connection, by contrast, seats with a wedge-like interference that turns drawbar pull into uniform radial contact around the full shank. That keeps the tool's centerline locked in place, so runout at the tip doesn't grow with overhang.
The second problem is vibration. Long tool assemblies amplify chatter, and a collet-gripped shank has only a series of line contacts to resist micro-motion. Tapered seats spread the load over a much larger conical surface, which raises the natural damping of the joint. The effect is most noticeable past a length-to-diameter ratio of ten, where a straight shank starts ringing and leaving a poor finish while a taper-shank tool remains quiet enough to hold size.
Repeatability matters just as much. Deep-hole work often calls for retracting to break chips and then re-entering the same bore. A standard shank may not return to exactly the same radial position, which widens the mouth of the hole and lets the drill wander. A taper re-centers itself every time it is drawn home, so the re-entry path stays true and the finished bore comes out straighter. It also transmits torque through the mating cone rather than relying on a single setscrew or collet squeeze, which reduces slipping and fretting under heavy feeds.
Inside the Production Line: How Precision Gets Built In
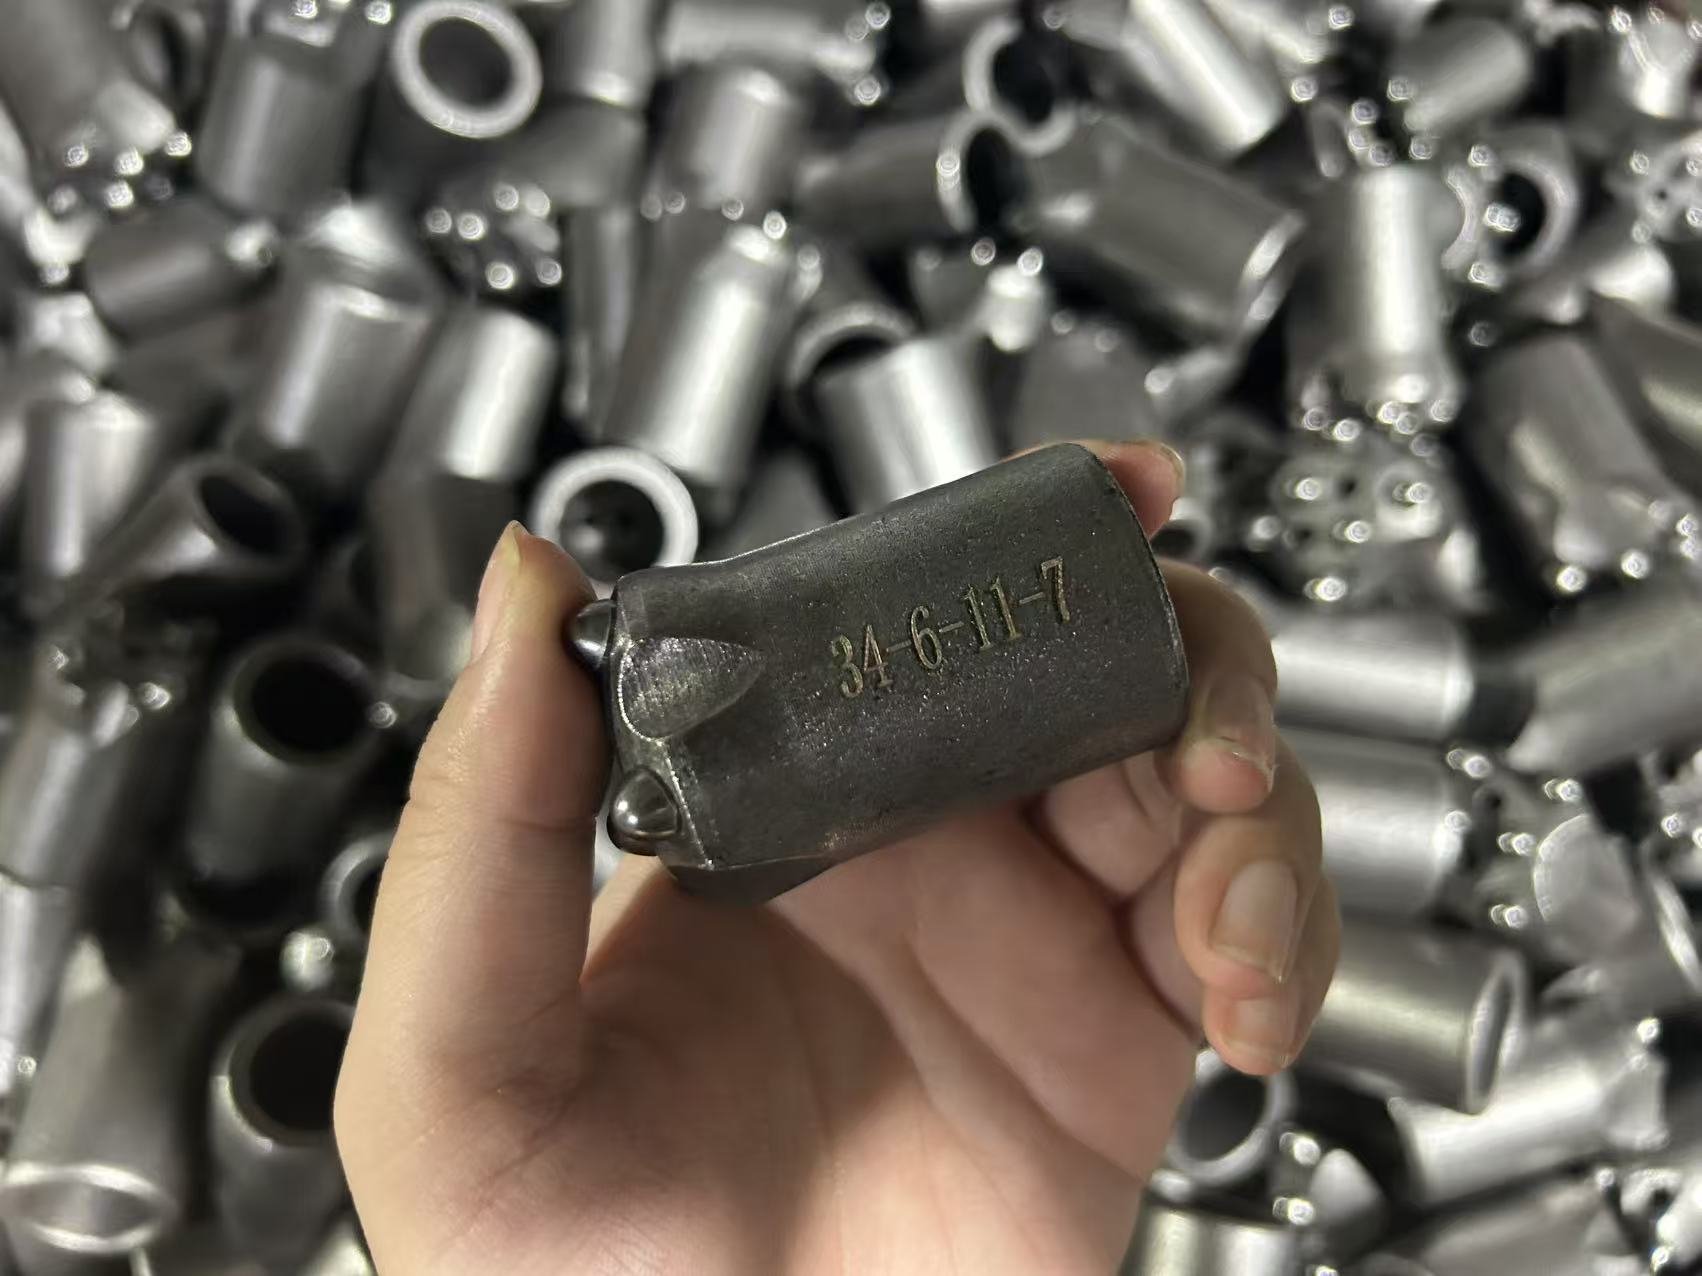
Precision on a production line doesn't happen by accident. It gets locked in long before the first component reaches the conveyor. Tooling engineers spend weeks refining cutting paths and clamping forces, running simulations that account for thermal expansion during long machining cycles. When the line finally starts moving, every station has a go/no-go gauge calibrated to tolerances tighter than a human hair—sometimes narrower than the width of a red blood cell. A part that measures off by just a few microns doesn't get reworked; it gets pulled and sent back to raw stock, because the entire downstream process assumes absolute repeatability.
What separates a decent factory from a truly precise one is how it handles the gray zones. Automated optical inspection catches most deviations, but the final call often falls to a veteran set-up operator who can feel a half-thousandth of an inch of runout through the vibration of a handwheel. That kind of tactile judgment can't be written into a work instruction. It gets passed down through months of shadowing, where a new technician learns to read the subtle change in cutting noise that signals a dulling insert before the control system flags it. Meanwhile, machine vision cameras snap hundreds of frames per second, feeding data back to adjust spindle speeds in real time—so precision isn't just built in once, it's actively maintained with every rotation.
Materials That Survive Abrasive Rock and High Torque
Rotary cutting heads, downhole hammers, and auger flights in hard formations don't just wear—they get gnawed away by rock fragments moving under hundreds of kilonewtons of thrust. The material has to resist micro-cutting from sharp mineral grains while absorbing torque spikes that would snap a purely brittle wear plate. That rules out a lot of conventional high-hardness steels.
In practice, the workhorse is often a composite: tungsten carbide buttons or inserts brazed into a tougher steel body. The carbide handles the scraping and gouging at the rock face, while the steel core flexes enough to survive torsional shock. For housings and auger casings, high-chromium white irons with 25 to 30 percent chromium are common because the primary chromium carbides blunt incoming abrasive particles instead of letting them cut grooves.
Hardfacing overlays matter too. Field crews often rebuild worn flights with chromium-carbide or tungsten-carbide wires, deliberately leaving the base metal slightly softer. That creates a sacrificial layer that erodes in a controlled way, while the hard cap takes the brunt. It's a balancing act—too much hard phase and the part cracks under high torque; too little and it washes out in a shift.
Case Files: Demanding Jobs That Rely on Our Drill Bits
In a tunnel boring project under a mountain range, the crew was pushing through abrasive granite with a mixed face of fractured rock. Standard bits dulled within hours, causing stoppages that cost six figures a day. Switching to our bits with a modified flute geometry and a carbide grade tuned for thermal fatigue let them finish the pilot bore two weeks ahead of schedule. The bits were far from the most expensive part of the rig, but they became the difference between penalty clauses and a bonus.
On an offshore platform, a maintenance team had to cut out seized bolts from a blowout preventer stack during a storm window. Every minute of downtime was tracked by the client's operations center. Our cobalt steel bits, with a split point that doesn't walk on curved surfaces, allowed them to extract all 38 fasteners without snapping a single one. The lead mechanic later said the bits "just kept eating" even as the drill motor overheated.
A geothermal drilling crew in basalt needed to set surface casing through a boulder field that kept deflecting the hole. Their previous bits would chip carbide at the first sign of lateral vibration. A switch to our four-flute design with an asymmetric land pattern held the path straight and survived repeated re-entries. The driller logged a 92 percent reduction in tripping time over the next three wells.
Custom Geometry and Thread Specs for Unusual Rigs
Oddball rigs rarely fit standard thread charts, so builders end up chasing rare pitches or cutting their own on a lathe. A 3D-printed thread gauge with a half-degree taper might save a weekend, but only if you trust the resin to hold tolerance. Aluminum mockups help too—cheap enough to scrap when the shoulder angle is off by a hair.
Geometry gets stranger when you mix metric and imperial on the same axis. A 16mm bore with a 1.5mm pitch sounds fine until you realize the mating part expects a 5/8-24 UNEF shoulder. That’s where a custom wrench flat thickness or a relieved groove makes the difference between snug and seized.
For truly weird stuff—think left-hand threads on a right-hand torque path, or double-start threads on a shock body—hand-drawing the profile beats CAD guessing. A Sharpie on a clean steel blank, then a smoke test with the actual component, reveals more in ten minutes than a full thread spec sheet ever will.
Field Feedback Loops That Sharpen Every New Batch
The most useful refinements never come from a conference room. They surface in the field, where a driver notices the latch feels stiff on a cold morning or a nurse realizes the new tray layout forces an awkward reach. These observations, gathered informally and often in passing, become the raw material for the next production run. By treating each batch as a draft rather than a finished product, teams build a quiet habit of listening to the people who actually handle the work.
A feedback loop only works if it closes quickly. Waiting weeks for a formal review means the context has already faded. Instead, short check-ins after each delivery—sometimes just a phone call or a shared photo with a comment—capture details that would otherwise vanish. The goal is not to collect more data, but to ask better questions: What surprised you? What did you have to work around? Those small frictions, once fixed, compound into smoother processes that no amount of internal testing could have predicted.
What makes this approach durable is that it does not depend on a single heroic insight. It runs on repetition and respect. When field teams see their notes reflected in the next batch—a redesigned clasp, a repositioned shelf—they start offering sharper observations without being asked. The loop tightens. Each cycle leaves the product a little more attuned to the real conditions of use, not the imagined ones.
FAQ
The tapered interface locks the bit and rod together under axial load, so energy transfer stays efficient even when the ground gets unpredictable. Quality manufacturers also match carbide grades and heat treatment to the specific rock formation rather than offering a one-size-fits-all tool.
Look for consistent geometry across batches, honest hardness ratings, and willingness to discuss failure modes. A dependable supplier will ask about your rig setup, air pressure, and rock type before recommending anything.
Underground mining, tunneling, quarrying, and geotechnical investigation all use taper connection bits. The common thread is a need for straight holes and predictable wear in abrasive or fractured ground.
Pay attention to the flushing grooves, face profile, and carbide button placement. Small changes there influence how quickly cuttings clear and how evenly the carbide wears, which matters more than the bit's overall appearance.
It is the difference between a bit body that survives repeated impacts and one that cracks early. A good heat treatment keeps the steel tough around the taper while leaving the carbide seats hard enough to hold inserts securely.
Yes, many top suppliers adjust the number of buttons, button shape, or flushing hole layout based on the rock hardness and rig parameters. Custom work often starts with a site visit or core sample review rather than a catalog pick.
Request a trial batch and track penetration rate, hole deviation, and bit life under normal operating conditions. Also confirm the manufacturer's inspection records for taper dimensions, as poor fit causes premature rod or bit failure.
Conclusion
Deep-hole drilling punishes weak links. The taper connection between bit and rod does more than hold parts together—it distributes thrust and torque across a wedged interface that resists loosening under vibration far better than a straight shank. On our production floor, that interface is ground and lapped to tolerances tighter than a few microns, then verified with coordinate measuring machines. The steel bodies are forged from nickel-chromium-molybdenum alloys and surface-hardened to withstand abrasive rock, while the carbide buttons are selected by grade and press-fitted under controlled load. Every batch leaves with a serial number tied to its machining history, so if a rig hits unexpected formation changes, we can trace exactly which heat lot and grinding wheel produced that tool.
We don't stop at standard catalog items. When a tunneling contractor in granite showed us a rig with an odd spindle nose and a need for 30% more water flow, we redrew the thread profile and flute geometry, then ran a short pilot batch within three weeks. Field reports from that job—along with hundreds of others—come back through a structured feedback loop. Tool wear patterns and penetration rates get logged, and the data feeds directly into the next production run's process parameters. That loop is why our bits have held up on 300-meter boreholes in fractured basalt and on high-torque directional jobs where others sheared threads. The result is not a generic "premium" label but a tool that matches the actual demands of the rock, the rig, and the crew.
Contact Us
Contact Person: Elma
Email: [email protected]
Tel/WhatsApp: +86 13738628777
Website: https://www.pulankagroup.com/