Inside a Toilet Paper Rewinding Machine Factory: How Precision Engineering Drives Production
2026-09-28
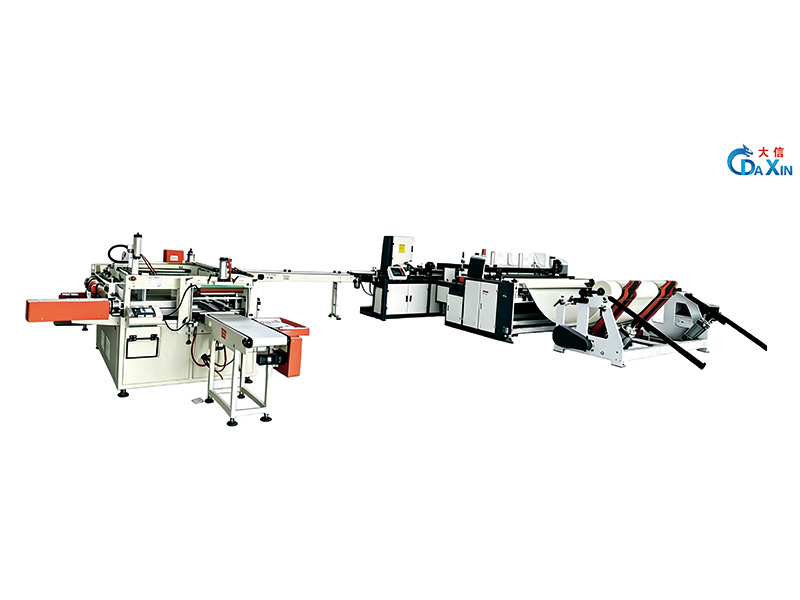
Most people picture a toilet paper factory as a blur of dust and spinning cardboard, but step inside a modern rewinding line and you'll find something closer to a Swiss watch: tension arms reacting in milliseconds, laser-guided slitters, and drive systems that hold tolerances most metal shops would envy. At DAXIN, that obsession with precision is built into every rewinder—because a half-millimeter drift can mean wrinkled sheets, snapped cores, or downtime that kills a shift. In this article, we'll look at how thoughtful engineering turns giant parent rolls into the neatly wound packs on store shelves, and why the details inside the machine matter just as much as the paper itself.
Where the Unwind Stand Sets the Pace for Every Roll
The unwind stand is more than a passive holder—it's the first actor in the line, setting the rhythm that every downstream roll follows. If the stand brakes too hard, the web fights you from the start, yanking tension spikes through the machine. Too loose, and you're chasing slack that folds into registration drift. Operators who treat it as a fixed point miss the control it grants: a properly tuned unwind lets you feel the substrate's character before it reaches the first print unit, making every roll start with intention instead of correction.
Consider the difference between a stand that releases uniformly and one that pulses with each rotation. The former lets the web enter tension control as a steady stream, so your dancer roller barely moves and splices land with predictable overlap. The latter forces constant micro-adjustments downstream, turning what should be a clean acceleration into a series of small lurches. That's why the unwind's mechanical health—brake pads, air shaft expansion, edge guide response—directly dictates how smoothly a roll can run. When the stand is dialed, the pace feels cooperative; when it's neglected, every splice, every speed change becomes a negotiation.
The real insight is that the unwind doesn't just set speed—it sets the ceiling for consistent output. A stand that runs true lets you push line speed without losing tension control, while a chattering brake caps your throughput long before the press or coater reaches its limit. Smart crews don't wait for wrinkles or web breaks to check the stand; they read its vibration with a hand on the frame and adjust pre-tension before the roll ever hits the first nip. That's how you make the unwind stand earn its place as the pacemaker of every roll that follows.
Core Alignment Tolerances That Prevent Wobble and Waste
Misalignment rarely announces itself until the first parts come off the line with chatter marks or a bearing runs hot. In rotating spindles and mold cores, the difference between a stable process and chronic scrap often comes down to a few microns of radial runout. Calling out a total indicated runout of 0.005 mm on a core seat instead of a loose clearance fit removes the subtle pivot point that lets the core orbit under cutting pressure. That wobble translates directly into non-round bores, uneven wall thickness, and tool wear that shifts over a shift.
The tolerance stack matters as much as any single number. If the locating bore, core shoulder, and retaining plate each carry a symmetric ±0.02 mm tolerance, the cumulative offset can exceed what the process actually tolerates. Switching to a position tolerance with a maximum material condition, or specifying a short taper pilot that self-centers, closes the gap between design intent and the as-built assembly. This approach costs little at the machining stage but eliminates the hidden waste of reaming, sorting, and hand-fitting parts later.
Alignment also affects material flow. In multi-cavity tools, a core that deflects slightly under injection pressure creates flash on one side and a thin wall on the other, driving up regrind and cycle time. Tightening the guide pin and bushing fit, or adding a tapered interlock, keeps the core on center without fighting thermal expansion. The result is not just less wobble on a dial indicator; it is fewer rejected shots, lower energy per part, and a tool that holds its alignment between preventive maintenance intervals instead of drifting after the first warm-up cycle.
Tension Zone Mapping: The Quiet Battle Against Sheet Stretch
When a sheet of metal is pulled past its yield point, it doesn't simply stretch uniformly. Certain regions deform more readily than others, creating hidden strain gradients that can lead to thinning, tearing, or unpredictable springback. Tension zone mapping emerged as a way to visualize those differences before they become defects. By tracking local strain fields with digital image correlation or grid-based measurements, engineers can pinpoint exactly where the material is working hardest and adjust tool geometry, blank holder force, or draw bead placement accordingly.
The real challenge lies in reading the map correctly. A peak in tensile strain near a corner might look alarming, but it can actually be a sign of healthy material flow if neighboring zones are balanced. In contrast, a mild but persistent stretch across a large flat area often causes more trouble, because it leaves the part with weak resistance to buckling and fatigue. This is why experienced process designers rarely chase a single number; they look at the contour shapes and gradients. A sharp transition between high and low strain almost always predicts a failure site, while a smooth, gradual change suggests the sheet is sharing the load the way it should.
Mapping also changes how teams communicate about forming problems. Instead of vague references to "too much stretch" or "not enough draw," they can point to a specific zone on the part and discuss what the strain path is doing there. It turns an abstract material behavior into something visual and actionable. Over time, the accumulated maps from past jobs become a reference library, allowing faster diagnosis of similar failures and smarter decisions about material grade, lubrication, and die surface finish. The quiet battle against sheet stretch is won not by brute force, but by knowing where the fight is actually happening.
Perforation Blade Tuning for Tear Strength and Softness
Adjusting the perforation blade is a hands-on balancing act between creating a clean tear line and keeping the material from feeling flimsy. The blade depth, angle, and spacing all influence how much force is needed to separate the sheet, so even a fraction of a millimeter can shift the result from a crisp snap to a ragged pull. Tuning typically starts with a baseline pattern, then runs test strips through the line while varying pressure and blade protrusion in small increments, checking both the tear energy and the surface touch after separation.
Softness doesn't only come from the base substrate; the perforation pattern itself changes how the sheet flexes and collapses in hand. A denser perforation can make the paper feel more supple because it creates more hinge points, but if the cuts are too deep, the sheet may tear during normal handling rather than only when intended. Conversely, shallow or widely spaced perforations feel stiffer and often produce a coarse, linty edge. Operators often adjust blade geometry to create a series of micro-cuts that weaken the fiber just enough for an easy, controlled tear without sacrificing the perceived body of the material.
Field adjustments usually rely on a quick feedback loop: tear a sample by hand, listen for the sound, and run a fingertip along the edge to feel for burrs or stray fibers. A well-tuned blade leaves a slightly feathered edge that feels soft rather than sharp or jagged. In many mills, the final setting is recorded as a combination of blade angle, penetration depth, and anvil pressure, then locked in for the production run—any drift in blade sharpness shows up within minutes as a change in tear resistance or a rougher edge, so periodic checks and light honing keep the output consistent.
The Adhesive Application Window That Stops Tail Unwinding
Everyone who has wrestled with a roll of tape knows the frustration: you set it down, and the free end curls back, sticks to itself, or worse, unwinds into a tangled mess. The adhesive application window targets exactly this headache. Instead of coating the entire backing with glue, the manufacturer leaves a precise, uncoated strip along one edge. That narrow margin becomes the tail's safe zone—no sticky residue to grab onto neighboring layers when the roll is at rest.
During production, the adhesive is applied in a controlled pattern, leaving a clean break line where the film meets the coated area. When you cut a piece and press the tail down, only the non-adhesive edge contacts the roll surface, so it stays put without bonding permanently. This means no more picking at corners or wasting inches of tape that have folded over on themselves. The tail peels away cleanly every time because the adhesive never crosses into that uncoated lane.
On the job site or in a shipping room, this window quietly saves minutes and temper. Rolls stay tidy on the bench, inventory remains usable down to the last wrap, and you never have to hunt for the starting point by feel. It's a small design choice, but once you've used tape that doesn't fight back, going back to fully coated edges feels like a step backward.
Servo-Driven Turret Indexing for Uninterrupted Log Flow
In high-volume log processing, even a half-second pause between infeeds creates a ripple effect that throttles throughput. The servo-driven turret indexing system eliminates this bottleneck by synchronizing rotation with the conveyor cadence. Instead of relying on fixed mechanical stops or hydraulic dwells, the servo motor continuously adjusts angular position based on real-time log spacing and diameter. This means the next pocket is already aligned before the previous log clears, keeping the material stream dense and predictable.
What sets this approach apart is how it handles irregular feed patterns. A conventional Geneva drive or cam indexer locks into a fixed step angle, forcing operators to batch logs by size or accept misfeeds. With servo control, the turret can shorten or lengthen each index on the fly, matching the natural variation of incoming timber. The result is fewer jams, less wear on transfer plates, and a steady discharge rate that downstream saws and scanners can actually rely on.
Maintenance teams also benefit from the absence of mechanical dwell adjustments. Servo parameters are stored digitally, so changeovers between log diameters take minutes rather than hours. Fault diagnostics report exactly which axis deviated from its profile, reducing troubleshooting from guesswork to a quick screen check. For mills pushing past 40 logs per minute, that combination of speed and adaptability is what keeps the line flowing without interruption.
FAQ
It takes massive parent rolls from the paper mill and rewinds them into the smaller logs you see on store shelves, cutting and perforating them to exact lengths while controlling tension so the sheet doesn't tear or stretch unevenly.
Even a fraction of a millimeter off in the winding tension or blade alignment can cause the paper to wrinkle, tear, or produce rolls with inconsistent diameters. Precision keeps every roll uniform so downstream packaging machines don't jam.
They use CNC-machined rollers, laser-aligned cutting stations, and automated sensors that continuously measure roll diameter and adjust speed or tension in real time. Regular calibration against certified gauges is also part of daily routine.
Parent rolls vary in moisture content, thickness, and tensile strength depending on the pulp source. The rewinder must adapt on the fly, often using servo motors and load cells to keep the winding tight and even without breaking the sheet.
A rotary perforation blade is timed with the feed rate. It is set to a sheet length—usually around 100 to 115 millimeters—and the machine's encoder ensures each perforation lands within a tolerance of a few tenths of a millimeter.
Yes, operators can change mandrel sizes, adjust winding length, and swap perforation heads. Changeovers might take fifteen to thirty minutes, but modern systems store recipes so the settings are recalled automatically.
Cameras and laser micrometers inspect roll diameter, edge alignment, and perforation spacing continuously. If a roll drifts outside spec, the machine either corrects itself or flags that log for rejection before it reaches packaging.
Older machines relied on mechanical cams and manual adjustments, so drift was common and speeds were lower. Today's servo-driven systems can hold tolerances at over 600 meters per minute, reducing waste and letting a small crew run multiple lines.
Conclusion
On the winding floor, the unwind stand is not just a feed mechanism; it establishes the rhythm for every parent roll that enters the line. Operators watch how the paper comes off the reel, adjusting brake pressure so that no sheet drags or snaps. Just downstream, core alignment tolerances are held to fractions of a millimeter. A core that sits even slightly off-center will wobble at speed, turning what should be a clean log into a source of edge waste. Then comes the tension zone mapping, a less visible but constant adjustment. Paper stretch is the enemy here; if the web pulls too tight through one section, the sheet loses its caliper and the finished roll feels thin in spots. The best lines run with a kind of quiet attention where every sensor reading is a small negotiation between speed and sheet integrity.
Perforation blades get tuned not just for cut depth but for the exact tear strength that matches a brand's promise of softness. Too deep and the sheet falls apart in your hand; too shallow and it tears ragged. The adhesive application window has its own timing problem: the glue has to land in the narrow moment when the tail is still moving fast enough to bond but not so fast that it skips. Servo-driven turret indexing ties it all together, rotating finished logs out and fresh cores in without pausing the line. That uninterrupted flow is what separates a machine that simply rewinds paper from one that produces rolls you can count on, roll after roll, without a tail unraveling in the package.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/