High Speed PVC Pipe Production Line Boosts Output and Product Quality
2026-11-19
Pipe producers have long faced a familiar trade-off: push output higher and quality usually slips. The latest high-speed PVC pipe production line from COMRISE turns that assumption on its head. In this post, we look at the design choices and real-world results behind a line that speeds up extrusion while tightening wall thickness control and surface finish.
What Actually Happens When a PVC Pipe Line Speeds Up
Inside a PVC line, an increase in flow velocity does not simply move the fluid faster—it rearranges the pressure profile along the pipe wall. The faster the stream moves, the more its kinetic energy climbs, and static pressure in narrow or slightly uneven sections can dip far enough to pull air through loose fittings or cause soft collapses in thinner-walled pipe.
That shift also turns small hydraulic shocks into sharper spikes. Because PVC has less give than materials like HDPE, a sudden speed change or valve closure sends a pressure wave through the line that can focus stress at joints, elbows, and threaded adapters. Over time those brief surges produce hairline cracks or loosened connections, even when the line holds normal operating pressure without complaint.
At the same time, faster flow increases turbulence and can leave charge accumulating on the non-conductive inner surface. Triboelectric charging is easy to overlook until a dusty or solvent-laden stream delivers a small arc near a fitting. Vibration also rises with velocity, so brackets and supports that felt solid at lower flow rates begin to work against the pipe, amplifying fatigue in places where the line changes direction.
Holding Wall Thickness Steady at Higher Throughput
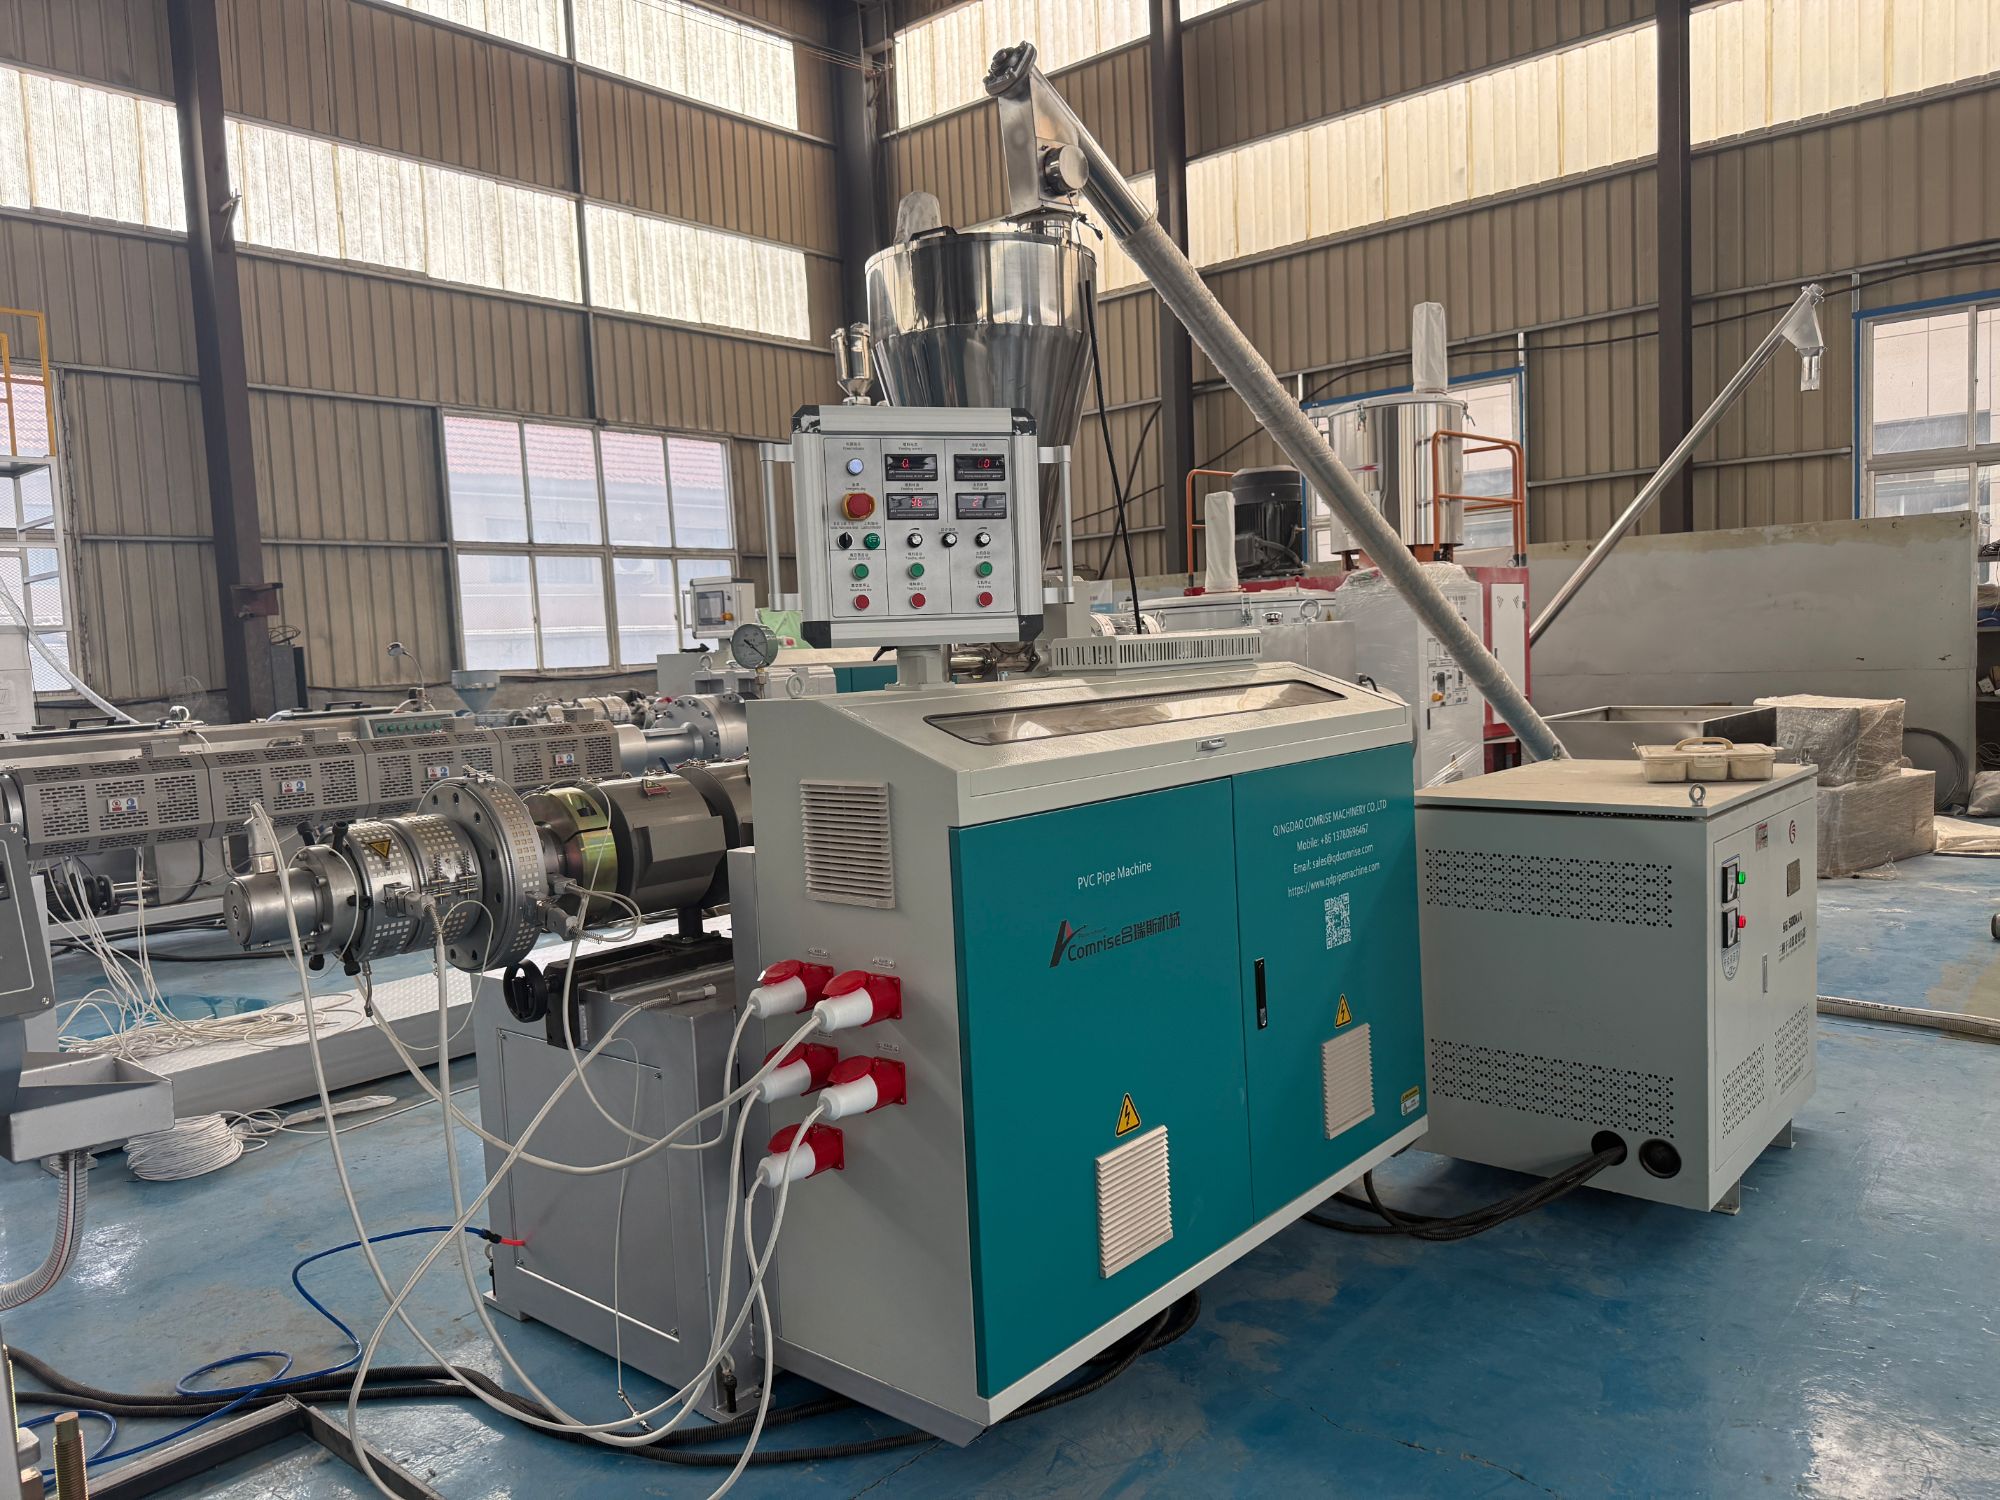
Running the line faster usually makes wall thickness drift, but this setup holds the reading steady without constant manual correction. The key change is keeping the melt pressure at the die entry flat while the screw speed ramps up, so the material sees the same flow conditions at every puller speed. As a result, the wall profile stays within a narrow band across the entire speed range rather than thinning out or bulging when the line accelerates.
What makes the difference on longer runs is that adjustments are made at the die and barrel temperature zones before the speed increase, not after the gauge starts moving. This reduces the usual cycle of speed-up, measure, correct, and scrap. Operators can step up throughput gradually and still maintain repeatable wall readings from the first meter after startup to the last reel change, which matters most when downstream cutting and handling rely on consistent tube geometry.
Screw and Melt Temperature Choices That Stabilize Quality
Actual melt temperature rarely matches the barrel set points once the screw starts doing its work. Shear heating in the compression zone can push the melt several degrees above the last zone, especially with worn screws or aggressive barrier designs. If you chase the set point instead of measuring what comes out of the die or nozzle, you end up adjusting the wrong variable. Stabilizing quality starts with knowing the real melt temperature at normal production speed, not just during a slow purge.
For many semi-crystalline materials, keeping the rear feed zone cooler than the front zones gives a more consistent feed wedge and avoids premature softening that leads to surging. The middle zones can carry most of the heat input, while the metering zone often works best just slightly below the target melt temperature to let screw rotation finish the heating. If degradation shows up as dark specks or gas bubbles, drop the metering zone or reduce screw speed before touching the rear zone.
Small changes in screw temperature, when a cored screw is available, can be more useful than large barrel shifts. A warm screw at startup can prevent cold-start torque spikes; once running, a slightly cooled screw can pull heat out of the melt film and narrow the temperature spread. Record the actual melt temperature along with the screw tempering setting and the recovery time. Over a few runs, that combination becomes a more reliable quality window than any single set point.
Cooling and Sizing Steps That Keep Dimensions on Target
Dialing in cooling rates often matters more than chasing a single machine setting. If the part skins over too quickly, the core keeps shrinking after the outer layer has already set, pulling flat surfaces into a slight bow or sinking bosses below the print line. Running coolant a few degrees warmer—or stepping the mold temperature in zones—can let the wall freeze from the outside in at a pace that leaves less locked-in stress.
Sizing fixtures earn their keep on thin ribs and long bosses. Instead of trusting the ejector stroke to leave every feature where the CAD model says it should be, a short post-mold hold in a water-cooled nest gives critical datums time to stabilize. The trick is holding the part just long enough to resist springback, but not so long that cycle time bleeds away without a measurable gain.
For tight bores and snap-fit edges, let the first few shots tell you where the process drifts after an hour of running. Measure, adjust the cooling circuit balance, measure again, and only then shift steel or tweak a holding pressure. That order keeps corrections based on thermal reality rather than a single cold-start reading.
Feeding and Blending Without Slowing the Line
On busy production lines, feeding and blending often become the quiet bottleneck. Instead of relying on batch hoppers that force downstream equipment to pause, plants can use continuous loss-in-weight feeders paired with short surge bins. The point is to keep material flowing at line speed while the controls trim each ingredient by weight, so the blender never has to wait for a weighment cycle to finish.
Changeover is where most systems lose pace. By moving blending into a small continuous mixer directly above the process intake, operators can adjust ratios on the fly rather than draining and refilling a large batch tank. Layering coarse and fine components through separate feed screws also prevents bridging and density segregation, which means the line holds its target rate even when raw material lots vary.
The equipment itself should support fast intervention without stopping the line. Feeders mounted on load cells with quick-release clamps and drop-out bottoms let maintenance clear a jam or swap a screw in minutes. If the feeding and blending setup is working properly, it becomes almost invisible on the floor—product stays within spec while the line keeps moving.
Scrap, Rework, and Downtime Signals Worth Watching
A climb in scrap often starts long before parts reach the reject bin. One dull insert can leave a burr that forces a downstream operator to compensate with an extra pass, and that adjustment quietly turns acceptable material into rework. Watching the ratio of scrap to rework by shift, rather than looking at a weekly total, makes it easier to spot whether the problem is a tool, a setup, or a training gap.
Rework carries useful information when it repeats on the same part number or the same feature. If a hole keeps getting reamed twice, the drawing tolerance may be unrealistic for the current fixture, or the inspection method is catching variation that the process cannot hold. Short handwritten notes from operators about why a part needed rework often reveal more than a dashboard metric because they capture the actual decision made at the machine.
Not all downtime announces itself with a red light. Small stoppages, sensor resets, jammed conveyors, and extended changeovers rarely get the same attention as a major breakdown, but they consume available hours just the same. Tracking these micro-interruptions for a few days usually surfaces one or two recurring triggers that can be fixed with a simple guard adjustment or a clearer work instruction.
FAQ
The main shift comes from synchronized extrusion, faster cooling and more precise haul-off. Together they let the line run at higher linear speeds without losing dimensional stability, so daily output rises while wall thickness stays consistent.
Only if the downstream equipment isn't matched to the extruder. In a properly designed line, faster cooling and closed-loop diameter control keep ovality and thickness within tight limits, so quality often improves rather than drops.
The vacuum sizing tank, multi-stage cooling baths and servo-driven haul-off usually matter most. They control shrinkage and pull force so the pipe can be cut cleanly at speed without deformation.
It depends on pipe diameter and formula, but many operators see 20 to 40 percent more throughput after upgrading to a well-tuned high-speed line, especially on smaller and medium diameters.
Not necessarily. Although total power draw rises, energy per meter often falls because the line spends less time running heaters and pumps for the same length of finished product.
Automated thickness measurement and feedback to the extruder and haul-off reduce manual corrections. The system can react in real time to slight material changes, which prevents drift during long production runs.
A full high-speed line fits new plants well, but many existing factories can also upgrade key modules like the cooling tank, cutter and control system to gain much of the same benefit without replacing everything.
Conclusion
Running a PVC pipe line faster usually invites a trade-off: more output but rougher surfaces, drifting wall thickness, or melt instability. On a well-tuned high-speed line, however, the real challenge shifts to managing how the material behaves once throughput rises. Barrel temperatures and screw speed have to be matched so the melt arrives at the die with enough homogeneity without adding unnecessary shear heat. Small adjustments in screw temperature profiles often do more for steady output than simply pushing the extruder harder, because overheating can degrade PVC and create dimensional variation that only appears downstream.
The downstream stages determine whether the higher speed actually holds up. Cooling and vacuum sizing must remove heat fast enough to lock pipe dimensions before sagging or ovality appears, while wall thickness stays consistent only if melt distribution remains even at the die. Feeding and blending also become more sensitive because minor inconsistencies in dryblend or regrind show up quickly when the line has less dwell time. Watching scrap rate, rework volume, and short stoppages gives a clearer picture than line speed alone, since those signals reveal whether the process is truly stable or just briefly outrunning its own control limits.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com