HIFU Transducer Factory: Inside Precision Manufacturing for Medical Devices
2026-08-18
Most people picture an operating room when they think of HIFU—but the real magic starts much earlier, on a factory floor where transducers are born. Here at Siansonic, we don't just assemble components; we obsess over every micron, every acoustic lens, every bond. In this post, I'll take you inside that process and reveal why precision manufacturing is the unspoken hero of modern medical devices.
Crafting the Acoustic Core: Piezoelectric Element Precision
Piezoelectric elements sit at the heart of any acoustic transducer, and their dimensional tolerance often separates a clean, stable signal from one riddled with spurious resonances. Achieving that precision starts long before assembly—raw ceramic batches are milled to sub-micron particle sizes, then pressed under carefully ramped pressure to avoid density gradients that would warp the resonant frequency. After sintering, each blank is lapped and polished until its thickness variation falls within ±0.005 mm, a figure that may sound generous until you consider how a single stray scratch can scatter acoustic energy into unwanted modes.
What makes this craft demanding is the feedback loop between geometry and electrical behavior. A slightly convex electrode face alters the field distribution, shifting the coupling coefficient enough to mute a target harmonic. Skilled technicians rely on interferometry and impedance analysis in tandem, iterating on edge chamfers or corner radii until the mechanical Q and electromechanical coupling factor lock into the design window. It is not purely subtractive work—sometimes a deliberate micro-texture on the back face helps break up standing waves, turning a brittle ceramic disc into a forgiving acoustic core.
Material selection adds another layer of nuance. Hard PZT formulations offer high sensitivity but demand tighter machining to avoid micro-cracking, while softer variants machine more readily yet drift under sustained drive. Many workshops therefore keep a small library of pre-aged elements, each tagged with its measured frequency drift over temperature. The final “acoustic core” is rarely just a part; it is a matched set of mechanical, electrical, and thermal tolerances that only reveals its quality when the first ping echoes cleanly back from a test phantom.
Cleanroom Assembly Protocols for HIFU Transducer Reliability
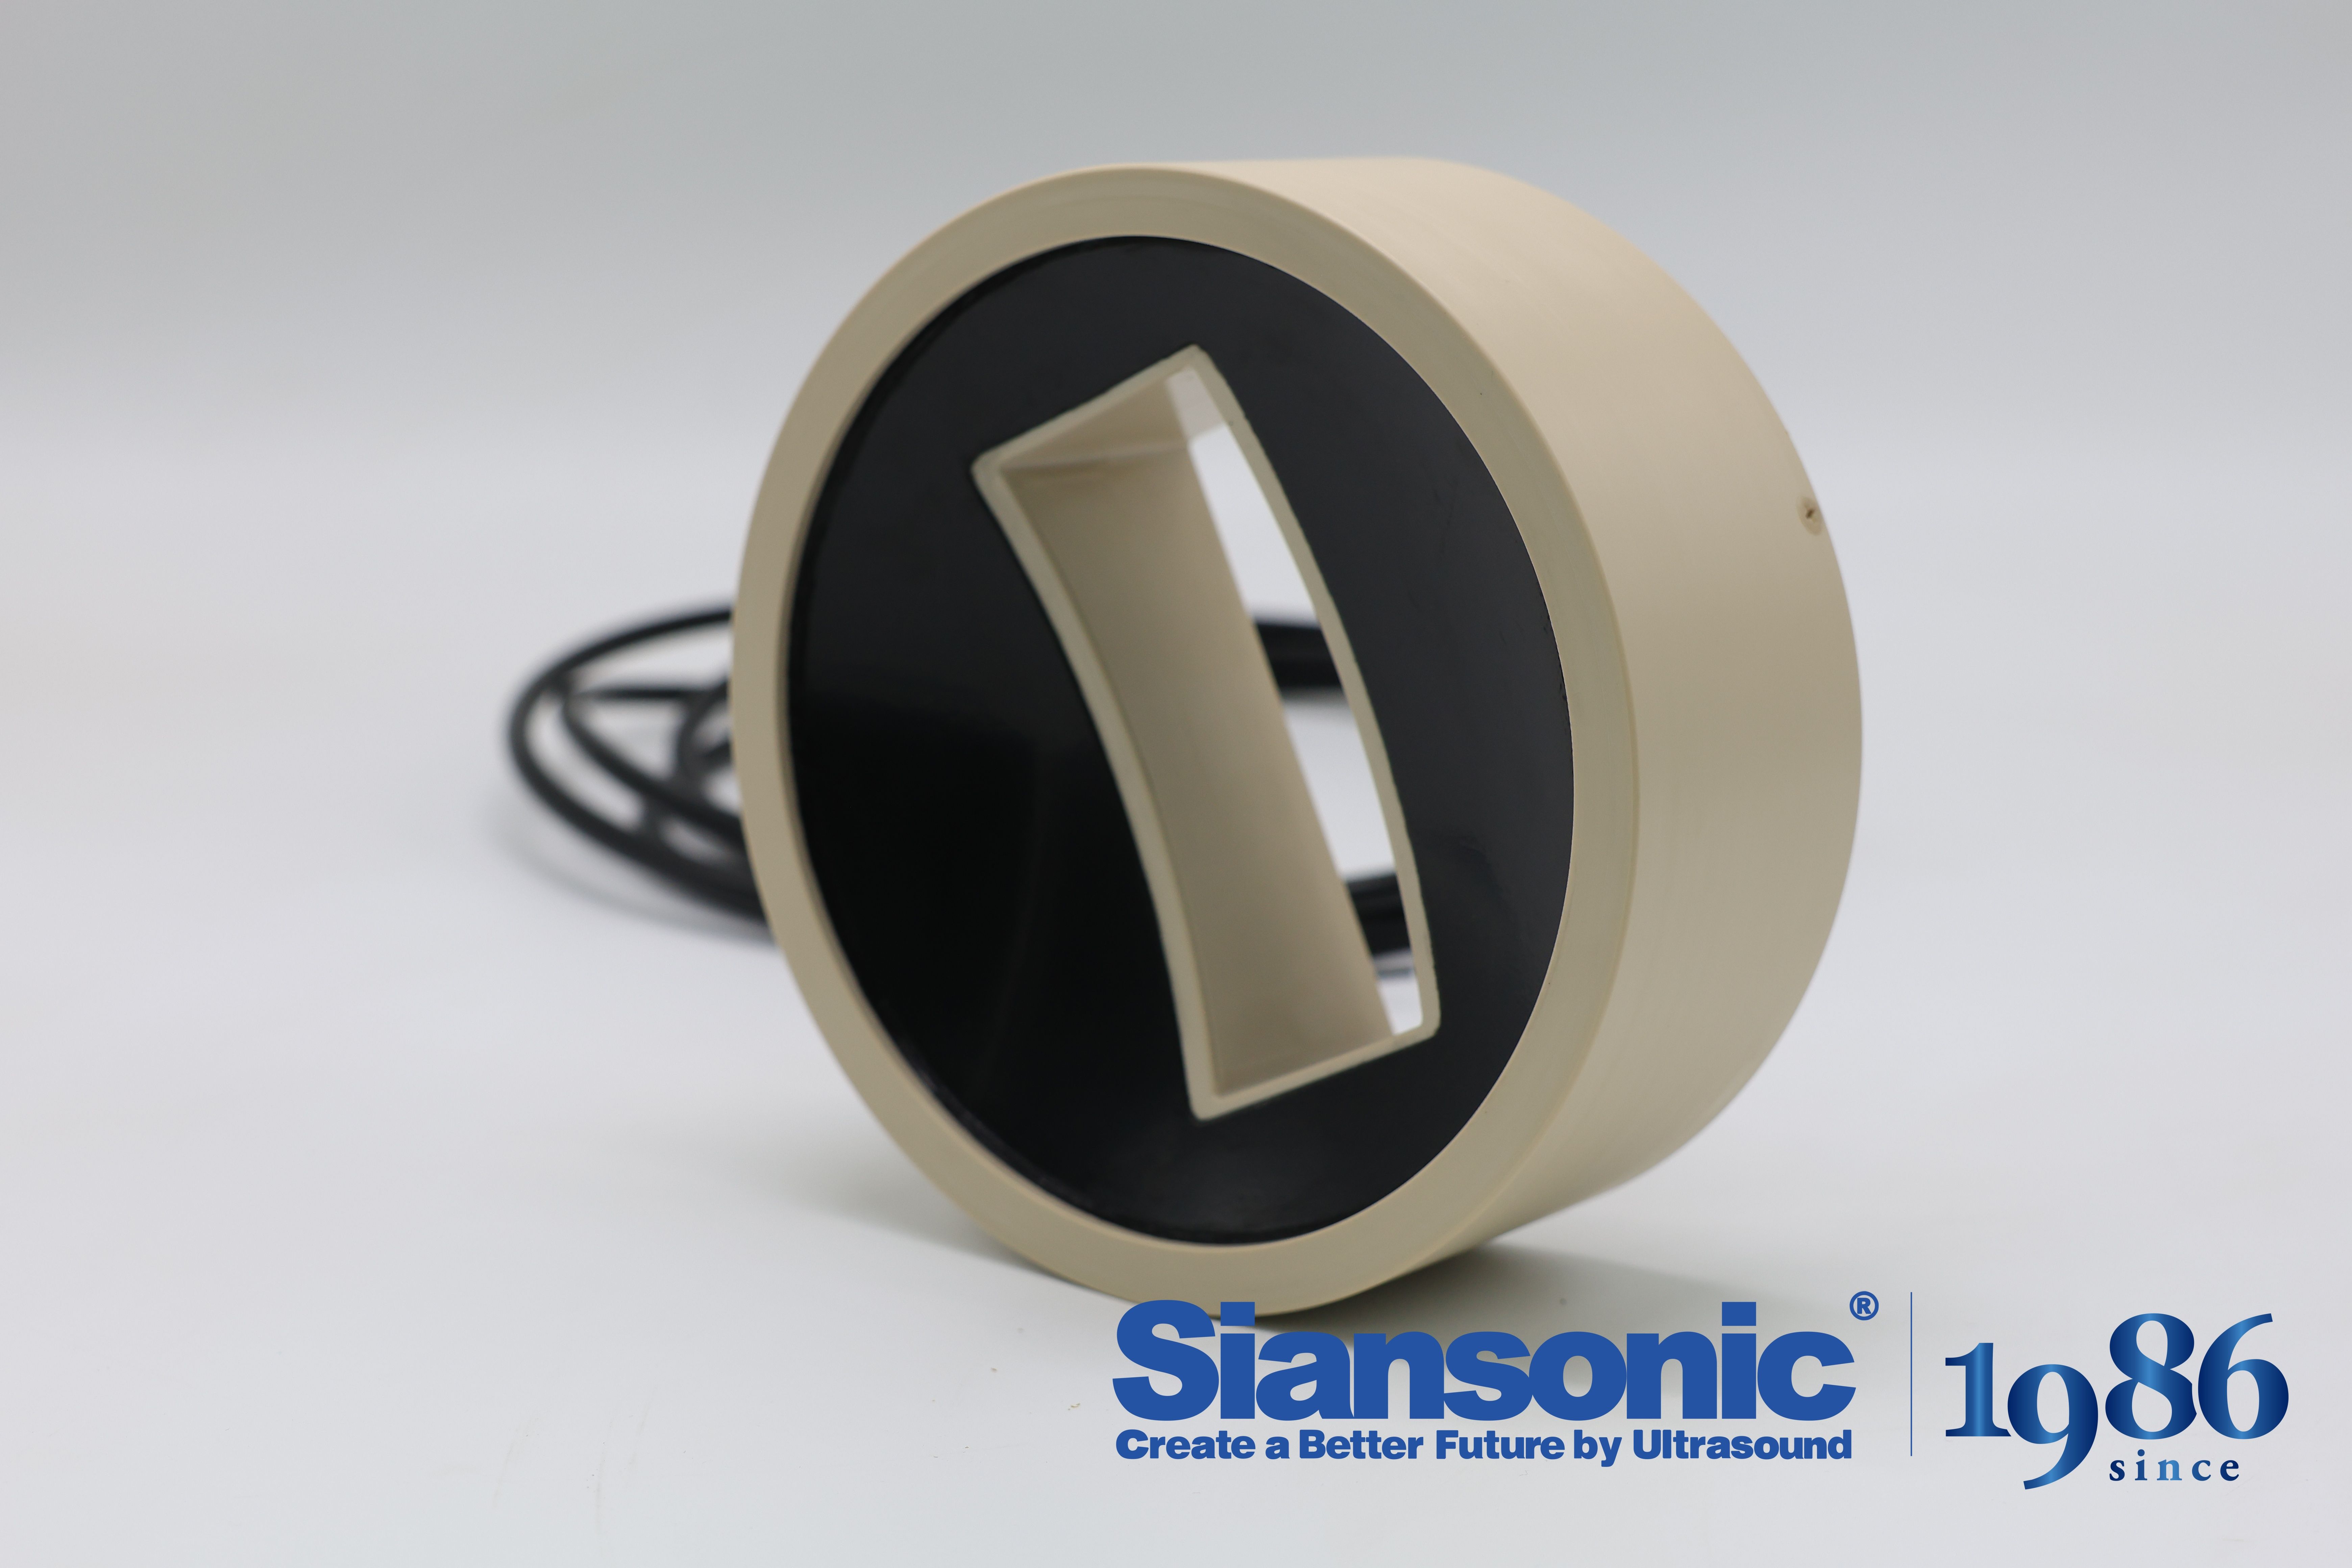
In HIFU transducer assembly, cleanroom protocols control submicron particles from the start because the bond interface between the piezoelectric wafer and the matching layer is extremely fragile. Any tiny fiber or metal debris can create localized stress concentration or voids under high-voltage drive, eventually evolving into dielectric breakdown or acoustic output drift. The working area is normally maintained at ISO 14644 Class 7 or better, with airborne particle counts verified periodically using a laser particle counter. Before touching the wafer, operators must pass through tacky mats and ionizing air showers, and wear powder-free nitrile gloves; all tooling and fixtures are wiped with isopropyl alcohol and vacuum degassed before entering the clean zone.
Bonding and curing steps are the key reliability points. Adhesives are prepared under controlled temperature and humidity, typically below 45% RH, because excess moisture changes epoxy cure kinetics and introduces microbubbles. Each adhesive layer between the backing, piezoelectric ceramic, and matching layer is applied by precision screen printing or spin coating to control thickness, then degassed under vacuum. Cure profiles are calibrated per material lot to avoid residual stress that can cause polarization decay. During assembly, a torque screwdriver is used to tighten the housing, preventing excessive compression of the piezoelectric ceramic; after the acoustic lens is bonded, scanning acoustic microscopy is performed to confirm there is no delamination or voiding.
Final cleaning and packaging also determine long-term reliability. After the acoustic stack is assembled, residual flux or grease on the transducer surface can migrate under high electric fields and create leakage current paths. Therefore, finished units are cleaned with semiconductor-grade solvent under clean conditions, vacuum dried, and then placed into static-shielding bags. At least one unit per batch is pulled for continuous power aging and thermal cycling tests to verify whether the cleanroom assembly protocol is effective. If early failure is found, particle counts, humidity logs, and operator actions are traced to improve line consistency through closed-loop changes.
Material Selection: Balancing Acoustic Performance and Biocompatibility
Choosing the right material for an implantable acoustic device is rarely a straightforward engineering decision. The material must transmit sound with minimal loss, yet it also has to sit inside living tissue for years without triggering inflammation, fibrosis, or rejection. Metals like titanium offer excellent mechanical stability and are well tolerated by the body, but their acoustic impedance is far higher than that of soft tissue, creating strong reflections at the interface. Polymers such as PDMS or parylene can be tuned to match tissue impedance more closely, improving transmission efficiency, but they often lack the long-term hermeticity needed to protect internal electronics from moisture and ions.
A practical compromise involves hybrid designs: a rigid core for the transducer, surrounded by a compliant encapsulation layer that both protects the electronics and reduces impedance mismatch. The encapsulation's thickness and elastic modulus can be adjusted to shift the resonant frequency of the assembly, which is critical because the device must operate within the audible range while surrounded by fluid and soft tissue. Materials like medical-grade polyurethane or thin-film silicon dioxide have been explored, each bringing trade-offs between fabrication complexity, acoustic transparency, and biological inertness. Testing under simulated body conditions, including temperature cycling and enzyme exposure, often reveals weaknesses that pure acoustic modeling misses.
Beyond passive transmission, some designs exploit piezoelectric materials whose acoustic properties can be altered with an applied voltage. This opens the door to active matching layers that adapt to changes in surrounding tissue - for example, after implantation, a thin fibrous capsule may form, altering the local acoustic environment. Selecting a piezoelectric ceramic or polymer with low hysteresis and stable performance in saline is then just as important as its initial acoustic match. Ultimately, the best choice depends on the intended implantation site, the expected device lifetime, and the acceptable level of in vivo variability, pushing developers to test multiple candidate materials in parallel rather than relying on a single specification sheet.
Laser Alignment and Bonding: Micron-Level Tolerance Control
Achieving micron-level tolerance in laser alignment and bonding starts with controlling the beam path and the workpiece position as one integrated loop. Instead of relying on static fixtures, production lines now use real-time vision feedback to measure the offset between the laser spot and the target pad, then correct the galvanometer mirrors or the motion stage before every bond. This closed-loop approach keeps lateral drift under a few microns even when ambient temperature shifts or the substrate expands slightly during a batch.
The bonding step itself introduces another set of variables that demand tight control. Laser power, pulse duration, and focal spot size have to be matched to the material stack so that the interface reaches the eutectic or solder melting point without overheating adjacent components. A small change in focus height—sometimes just five microns—can widen the heat-affected zone enough to weaken a neighboring wire bond or distort a polymer layer. Operators tune the process window by mapping the relationship between laser energy and post-bond shear force, then lock those parameters into the recipe with automatic drift compensation.
In practice, micron-level tolerance control is less about a single perfect alignment and more about repeatability across thousands of cycles. That means monitoring the beam profile at scheduled intervals, cleaning the optics before contamination can scatter the spot, and using telecentric lenses to eliminate perspective error in the vision system. When these elements are combined, the line can hold placement accuracy within ±2 µm and deliver bonds that pass pull tests with little rework.
Testing Every Transducer: Acoustic Output and Thermal Validation
Every transducer that leaves the line gets run through a hydrophone scan, not just a spot check. We map the beam profile across multiple planes and record peak negative pressure, pulse intensity integral, and mechanical index under worst-case drive conditions. If a unit drifts by more than a few percent from its reference calibration, it is pulled and re-tuned before it goes anywhere near a patient.
Thermal behavior is handled with the same rigor. Thermocouples are bonded to the lens and housing while the transducer runs at maximum output for a sustained period. We look at surface temperature rise, internal heating near the matching layers, and how quickly the assembly cools after power is removed. Those numbers have to fall well below the regulatory limits, but we also track them unit-to-unit so that a gradual shift in a vendor's ceramic stack doesn't slip through.
The point is simple: acoustic output and thermal performance are not batch-level assumptions. Each array, each cable, each lens gets its own record. If something looks borderline, it doesn't ship.
Custom HIFU Designs: From Prototype to Regulatory-Ready Production
A custom HIFU build rarely starts with a clean set of specs. More often it begins as a rough sketch on a whiteboard or a clinician describing why an off-the-shelf transducer keeps missing the mark. Early prototypes lean hard into 3D-printed housings and borrowed amplifier channels just to map the acoustic field. The point at this stage is not to make something pretty; it is to find out quickly whether the focal zone can stay tight enough without cooking the surrounding tissue. I have watched teams shrink a planned treatment volume by nearly half after the first benchtop thermocouple test showed too much energy spilling past the target margin.
Once the acoustic stack stops changing every other day, the focus shifts to a different kind of rigor. Materials that were fine for a lab demo suddenly need full biocompatibility data and batch traceability. Cable routing, strain relief, and connector locking get reworked because an auditor will care about those details just as much as the transducer output. We keep a running design history file that records why each change was made, not just what changed, so that twelve months later nobody has to guess at an abandoned design path.
By the time a custom HIFU device reaches pre-submission, the prototype and the paperwork have to tell the same story. Test reports need to come from verified fixtures, risk analyses need to cite real failure modes from accelerated life testing, and the assembly process has to produce the same output more than once. The real deliverable is not a single working unit. It is a design that can be traced from initial requirements through final inspection without a reviewer stopping to ask where a number came from.
FAQ
You usually walk into a cleanroom split into zones for wafer dicing, bonding, housing assembly, and final acoustic testing. Operators work at stations with vision-guided alignment tools, and each transducer goes through a step where the piezoelectric element is precisely centered on the matching layer before the housing is sealed.
Even a few microns of misalignment in the piezoelectric array can shift the focal point enough to damage healthy tissue instead of the targeted lesion. Factories hold tolerances tighter than a human hair because the beam shape, acoustic power, and safety margins all depend on that mechanical accuracy.
Most production lines rely on modified PZT ceramics, but some specialized devices use single-crystal relaxor materials or 1-3 piezocomposites. The choice depends on the operating frequency, required bandwidth, and how much thermal stress the element must survive during repeated high-power pulses.
Every unit goes through multiple checkpoints. First, impedance and capacitance are measured to catch wiring or bonding faults. Then a hydrophone scan maps the acoustic field in a water tank, and thermal imaging under load reveals any hot spots that could lead to premature failure. Only after these pass does the transducer get a final acoustic output certificate.
Yes, and it is more common than people assume. A factory might produce one batch with a 60 mm focal length for dermatology, then switch to a 120 mm focal length for uterine fibroid therapy. Custom housings, connector types, and even non-spherical lens shapes are all possible, but each design change requires revalidation of the acoustic field.
The biggest issue is keeping the adhesive layers uniform when you move from hand assembly to automated dispensing. Curing ovens have thermal gradients that can warp backing layers, and piezoelectric ceramics from different supplier lots often vary in resonant frequency by a few percent. Factories solve this by sorting elements into matched sets and using closed-loop alignment feedback during bonding.
They run accelerated life tests where the transducer fires thousands of high-power bursts in a water bath while monitoring acoustic output, impedance, and surface temperature. Some factories also cycle the ambient temperature between 5°C and 60°C to simulate years of use in different clinical environments. A drop in electroacoustic efficiency beyond a set threshold means the design fails the durability gate.
Automation handles the most delicate steps, such as dispensing epoxy in a precise spiral pattern or soldering lead wires to the piezoelectric disc with laser heating. Vision systems check the alignment after each operation, so a robot can reject a misaligned element immediately rather than letting it reach final test. That said, experienced technicians still do final acoustic tuning because it requires judgment calls that robots are not yet good at.
Conclusion
Inside a HIFU transducer factory, precision is not just a goal—it's the entire operating system. The process begins with the acoustic core, where piezoelectric elements are machined and tuned to exact resonant frequencies. Every crystal is inspected under high magnification for micro-cracks and thickness uniformity, because even a 0.01 mm deviation shifts the focal zone. Cleanroom assembly then takes over, with operators in full gowns handling components under laminar flow. Static control, particle counts, and humidity are monitored continuously, since a single stray fiber can create a hot spot during high-intensity ultrasound delivery. Material choices are equally strict: PZT-8 or single-crystal piezoceramics offer high electroacoustic efficiency, while matching layers and backing materials must pass ISO 10993 biocompatibility tests. No adhesive is allowed to outgas or degrade after repeated sterilization cycles.
Alignment and bonding rely on laser interferometry and automated optical inspection to hold micron-level tolerances. The transducer's acoustic lens is positioned relative to the piezoelectric array with a repeatability of ±2 microns, ensuring the focal point lands exactly where the surgeon plans. After bonding, each unit enters a rigorous validation loop: acoustic output power, beam profile, and electrical impedance are measured in a water tank, while infrared cameras map thermal rise during continuous wave operation. Custom HIFU designs follow the same pipeline, but with added documentation for regulatory submission—traceability matrices, risk analyses, and process validation reports are generated in parallel. The result is a transducer that performs identically from prototype to serial production, whether it targets uterine fibroids, prostate tissue, or neurological pathways. In this environment, precision manufacturing is not a marketing phrase; it is the only way to guarantee patient safety and clinical repeatability.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/