China PPR Pipe Machine: A Practical Buyer's Guide for Consistent Production
2026-10-17
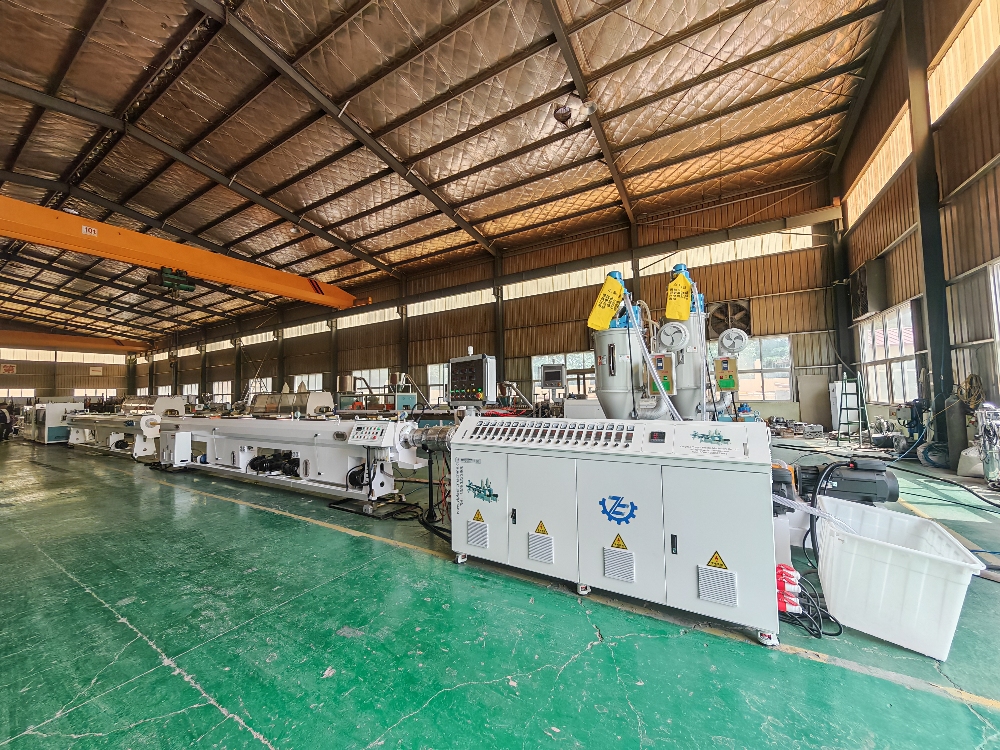
Choosing the right China PPR pipe machine often feels like navigating a sea of similar specs and bold claims—yet the difference between consistent daily output and costly downtime comes down to details most buyers overlook. In this guide, we cut through the noise to highlight what actually matters for reliable production, from screw design and temperature control to after-sales support. Along the way, you'll see why manufacturers like Yongte have earned a reputation for keeping lines running smoothly rather than just selling equipment. If you're tired of guesswork and ready to invest in machinery that delivers repeatable results, read on.
How to Spot a PPR Line That Will Hold Tolerance at High Output
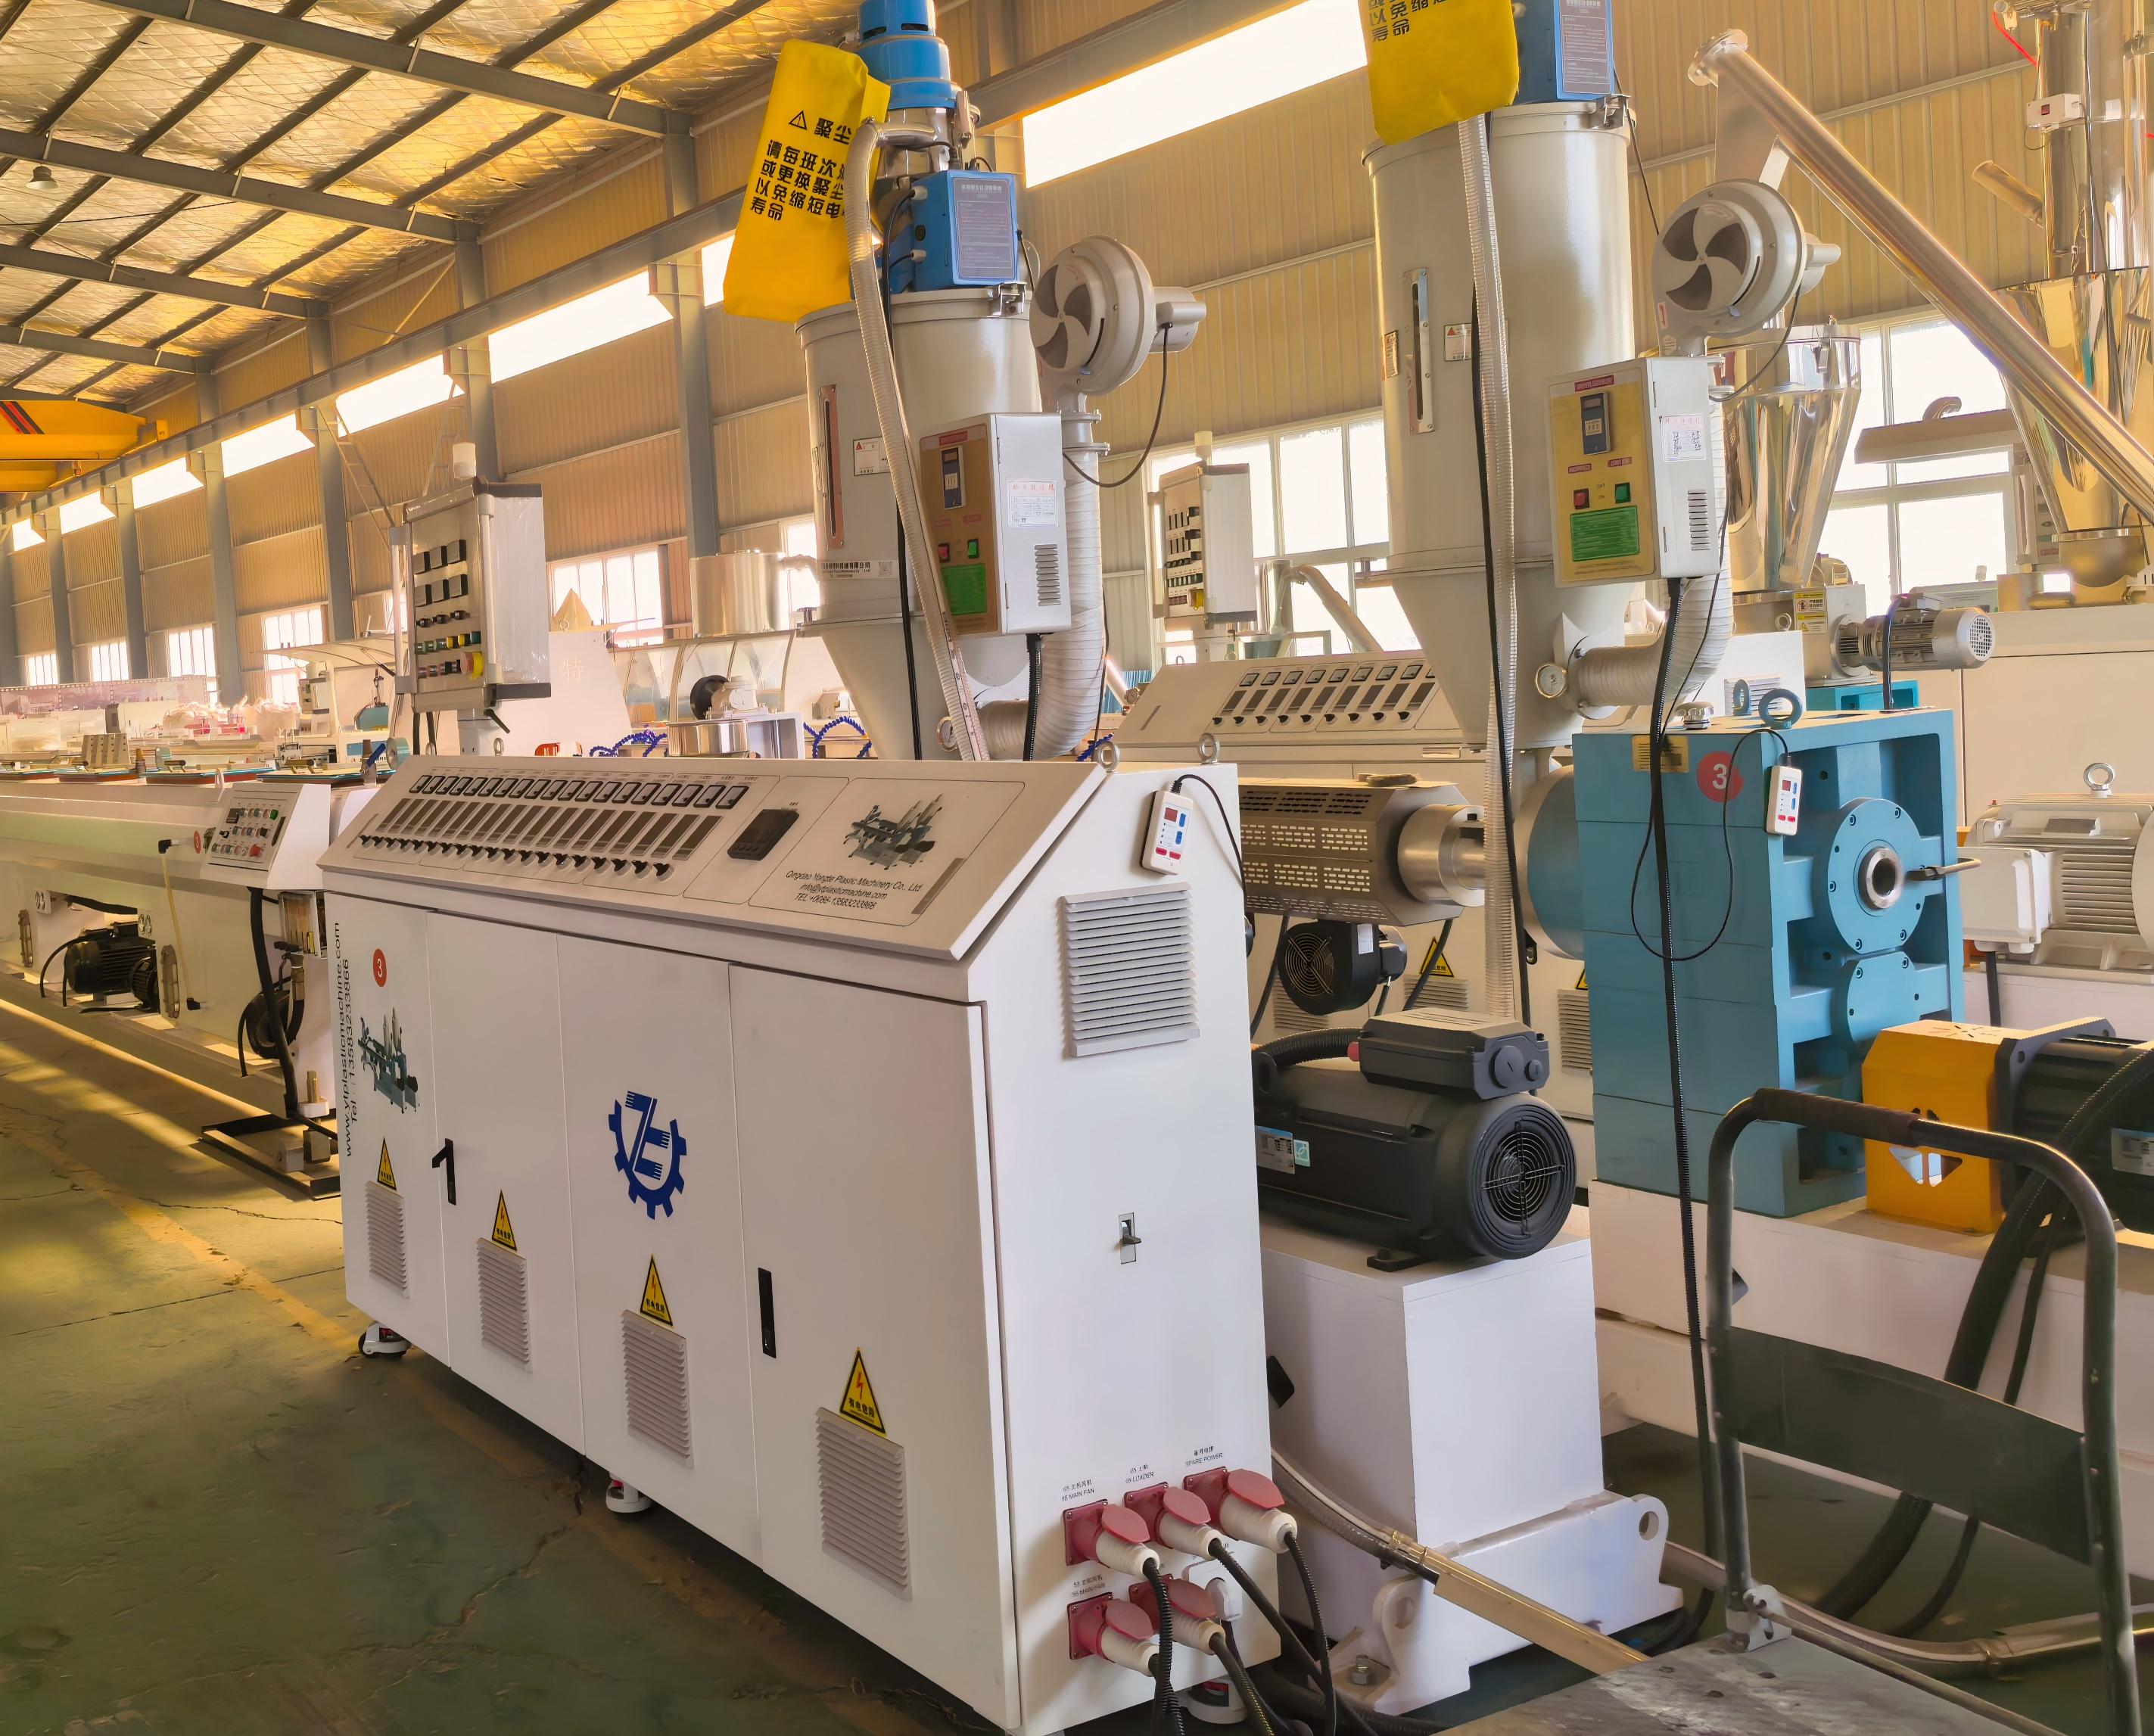
A PPR extrusion line that holds tight dimensional tolerance at high throughput rarely advertises it outright. Instead, look for subtle engineering choices: the barrel cooling zones should be oversized rather than just adequate, with independent PID control loops per zone and melt temperature variation kept under ±1.5°C during rapid screw speed changes. Watch the die head geometry—lips with adjustable flex-lip bolts and a short, straight land length after the final taper tend to distribute melt pressure evenly, reducing die swell fluctuation that usually wrecks ovality when output climbs.
The haul-off and vacuum calibration tank tell you more than the extruder. A line built for speed uses dual-stage vacuum calibration with separate circuits for the first 300 mm and the remaining cooling length, plus an air knife before the first sizing sleeve to prevent water carryover. The haul-off itself should have a direct-drive servo motor with closed-loop tension feedback, not a simple open-loop VFD pulling through a rubber belt. If you can request a live run, ask to see diameter data logged at 3-second intervals while the line speed jumps from 60% to 95% of rated output—tolerance should recover within 20 seconds without manual operator tweaks.
Finally, check the spare parts list and the control software. A line meant for stable high-output work keeps multiple interchangeable screw and barrel sets for different material grades, and its HMI will show melt pressure normalized by screw RPM rather than raw pump speed. Avoid machines that rely on downstream thickness correction loops to fix upstream variability; that approach masks problems at moderate speed and fails entirely once you push past 85% of rated capacity. Real capability shows up in the baseline variation before any feedback correction kicks in.
The Parts That Wear First and What That Means for Your Schedule
Most riders assume the frame gives out first, but it rarely does. In practice, you'll notice wear patterns on the parts you touch and move most often: grips, brake pads, chain, and tires. Each has its own timeline, and once you learn to read those subtle cues, you stop guessing about maintenance and start planning it.
Grips typically need attention every six to twelve months depending on your hand pressure and weather exposure. If you feel them getting slick or see cracks forming near the clamps, don't wait for a full failure. Replacing grips early prevents hand fatigue and keeps your control predictable. Brake pads wear faster on the rear wheel if you habitually drag that brake, and they can go from okay to metal-on-metal in a couple of hard rides once the wear indicator disappears.
Chains stretch gradually, but the effect on your cassette and chainrings is sudden if you ignore it. A simple chain checker costs less than a coffee and tells you whether you're at 0.5 or 0.75 percent wear. Swap the chain before it hits 0.75 and you might get three cassettes per chainring. Tires round out the early-wear group: check for squared-off profiles or tiny cuts that expose casing threads. If you schedule twenty minutes every two weeks to inspect these four areas, your longer service intervals become far more predictable, and you'll rarely face a surprise repair on the trail or road.
Sizing the Extruder to Your Real Production Goals, Not the Catalog
Plenty of processors start by flipping through a catalog, circling the model with the biggest hourly output or the one their competitor happens to run. That's backwards. The catalog tells you what a machine can do under ideal conditions, not what your floor will actually demand. Start instead with the numbers that matter to your operation: how many pounds or kilograms you need per shift, how often you change materials or colors, and whether your runs are long and stable or short and fragmented. A machine sized for peak theoretical throughput often ends up running at 40% capacity, wasting energy, wearing screws unevenly, and making every changeover slower than it should be.
Think about the melt quality you actually need, not just the pounds per hour. If you're running a shear-sensitive resin or a heavily filled compound, a smaller screw turning faster might degrade the material, while a larger diameter at lower RPM keeps the melt cooler and more consistent. Look at your real production window: do you need 24/7 continuous output, or do you need to switch from one job to the next three times a day? A catalog may tout a 150 mm extruder for high output, but if your runs average 300 kg and you change materials twice daily, that machine's startup purge alone could eat your margin. Match the screw diameter, L/D ratio, and drive power to the sweet spot where your typical job runs at 70–80% of the machine's comfortable capacity, not its redline.
The smart move is to bring real data to the equipment conversation. Pull your actual production logs: average order size, material types, scrap rates from previous lines, and how often you fight temperature overshoots or screw recovery delays. Then ask the vendor to run a trial with your material, your tooling, and your cycle targets. You don't need the machine that looks best on a spec sheet. You need the one that hits your throughput, melt quality, and changeover costs without forcing you to redesign your entire workflow around somebody else's defaults.
What Chinese Suppliers Won't Always Tell You About Delivery and Support
Many suppliers will quote you a delivery window that reflects a perfect production run, not the messy reality of material delays, mold adjustments, or last-minute quality fixes. Small orders are especially vulnerable to being pushed aside when a larger client comes along, leaving you to chase updates through time-zone gaps and vague WeChat replies.
Once the final payment clears, the support dynamic often shifts. Unless you've negotiated an explicit service-level agreement, don't assume that troubleshooting a faulty batch or getting replacement parts will be fast—or free. Many factories lack overseas technical staff, so you may end up paying for return shipping and waiting weeks for a resolution.
Custom packaging, special certifications, or minor design tweaks are often presented as easy add-ons during the sales pitch. In practice, these changes can trigger unannounced fees, longer lead times, and even minimum order quantity bumps that only surface after you're committed. Ask for a line-by-line breakdown of any modification before you sign off.
Running a Trial Batch: What to Watch Beyond the Surface Finish
A smooth surface can easily fool you into thinking a trial batch is ready for production, but the real test lies in how the parts hold their dimensions across the entire run. Instead of measuring just one or two pieces, check critical features on the first, middle, and last parts off the machine. Tool wear, thermal drift, or a slight change in material hardness often shows up as a gradual shift in size, not as a sudden failure. Compare actual measurements to the CAD model at multiple points, and pay attention to any mating surfaces or hole positions. If a part fits the gauge on Monday but not on Wednesday, the process is not stable enough to scale.
Residual stress is another silent problem that no surface finish will reveal. A part that looks perfect today can warp or crack after a few days on the shelf, especially if it was machined aggressively or formed with uneven pressure. Run a couple of trial pieces through a simple stress-relief step or a light functional load test before you sign off. Also track process repeatability, not just part quality: cycle time, tool change intervals, and even the way operators load fixtures can shift between the trial and full production. Write down every small deviation, because a five-second delay or a slightly warmer coolant tank often predicts a much larger issue when you scale up.
Keeping a PPR Machine Profitable After the First 10,000 Hours
After 10,000 hours, the real profit leaks come from small, often-ignored parts: worn heater plate coatings, dull trimmer blades, and temperature sensors that drift out of calibration. Instead of waiting for outright failure, replace these items on a cycle-count schedule, not a calendar one. A $40 sensor swap can prevent a rejected batch that costs $900 in pipe and labor.
Pay attention to actual cycle time, not just the number of joints completed. If operators are adding an extra 10 seconds per weld to compensate for a sluggish clamp or a weak heating element, that hidden downtime adds up fast. Rebuild pneumatic cylinders at the first sign of slow movement, and check hydraulic oil viscosity before it degrades to the point of slowing carriage travel. Track energy draw per fused joint; an upward trend often points to insulation breakdown or a failing contactor long before a breakdown.
Profitability after 10,000 hours also depends on what you are not doing. Run a one-week log of scrap, rework, and manual overrides. Frequently the machine itself is fine, but the pipe supports or workholding have shifted slightly. Re-leveling the frame, shimming the carriage back to square, and re-torquing the clamp bolts can restore repeatability without buying new components, keeping the margin on every joint where it should be.
FAQ
Focus on the melt pump and screw design. Ask for a detailed screw drawing and check if the supplier uses a barrier screw with a dedicated mixing section. Request a recorded trial run with your own feedstock, not their pre-dried resin. Watch for pressure fluctuation at the die head—anything above ±0.3 MPa during a 30-minute run usually signals inconsistent output.
The vacuum calibration tank and haul-off are frequent weak points. Undersized vacuum pumps cause poor diameter control when room temperature rises, and weak haul-off belts slip on smooth pipe surfaces. Specify at least two vacuum pumps with independent circuits and check the belt contact length before ordering.
Ask for a live video of the exact machine model running for at least 20 minutes. Request close-up shots of the gearbox temperature, die head pressure gauge, and the cut surface of a freshly produced pipe. A grainy pre-recorded video or a refusal to show the gearbox area usually indicates a machine that overheats under load.
The difference almost always sits in the screw and barrel metallurgy, bearing brands, and PLC components. Cheaper machines use nitrided 38CrMoAl screws that wear out in 18 months with filled compounds, while better lines use bimetallic barrels and SKF or NSK bearings. Ask for the specific steel grade and bearing part numbers in writing.
Insist on a power meter reading during a trial with your target pipe diameter and wall thickness. Compare the kWh per kilogram of finished pipe, not per meter. Many suppliers quote energy use at low output speeds. A realistic figure for a 63mm SDR11 line is around 0.35–0.45 kWh/kg including all auxiliaries.
Mismatched cooling between the first and second vacuum tanks. If the first tank is too short or the spray nozzles are partially clogged, the pipe's skin freezes unevenly before it enters the second tank. Check the nozzle layout diagram and clean the filters weekly—ovality often appears only after a few hours of stable running.
Get a written list of spare parts with part numbers for the first two years, including heater bands, SSR relays, and the specific PLC model. Specify a response time for video-based troubleshooting (e.g., within 4 hours during Chinese working days) and ask for the commissioning engineer's flight ticket to be included only after your factory has water, power, and resin ready.
Pull the screw and inspect the flight tips for wear, especially in the compression zone. Run the machine unloaded and listen for gearbox whine—louder under reverse rotation usually means bearing damage. Request the full maintenance log, and if it is missing, assume the barrel heater bands have uneven hot spots and budget for replacement.
Conclusion
Buying a PPR pipe line from China is less about horsepower on the spec sheet and more about matching the screw geometry, barrel heating zones, and downstream puller to the wall thickness you actually plan to run every day. Lines that hold tolerance at high output tend to have a melt pump and a vacuum calibration tank long enough to cool the pipe under tension, not just a shiny touchscreen. Watch the wear items early: screw and barrel in the feed zone, the die lips, and the calibration sleeves are usually the first to drift. If your supplier cannot quote replacement lead times for those before you pay, your schedule will own you later. Size the extruder for the diameter and output you really need, not the biggest catalog number, because an oversized screw running slow creates residence time and burns stabilizer, while an undersized one forces you to overheat the melt just to hit a rate.
Delivery and support are where several Chinese suppliers get vague, so ask for a written commissioning checklist and the name of the engineer who will handle after-sales video calls. A trial batch should not end at checking gloss or diameter; cut samples from the first and last ten meters, measure ovality after cooling, and run a hydrostatic burst test on at least one joint. Surface finish can look perfect while wall thickness is uneven under the skin. After the first 10,000 hours, profitability comes from disciplined preventive maintenance: change filters and check heater bands before they fail, keep the vacuum pump water clean, and track energy per kilogram instead of just output. The lines that stay profitable are the ones where operators log small drifts early, not where management waits for a breakdown to negotiate spare parts.
Contact Us
Contact Person: Ms Qin
Email: [email protected]
Tel/WhatsApp: 8613583233866
Website: https://www.yongteplast.com