China Performance Cylinder Head Upgrades for Serious Engine Builds
2026-11-03
Serious engine builders chase every last cfm, but the real gains start where air meets metal. China performance cylinder head upgrades have moved far beyond budget copies—today they’re a calculated choice for builders who demand repeatable flow numbers and rock-solid metallurgy. DDR takes that shift further with CNC-ported castings, upgraded valve seats, and deck surfaces that survive sustained boost. Before you bolt on another turbo or swap cams, the head is often the quiet bottleneck. This guide breaks down what to look for in a performance cylinder head, why Chinese manufacturing has changed the value equation, and how DDR's approach helps serious builds hold power without cracking under pressure.
The Hidden Airflow in Chinese Castings
Most buyers judge a casting by its surface, but the real story often unfolds in the microscopic channels and voids left by escaping air. In Chinese foundries, these hidden airflow paths—whether from trapped gas during pouring or from sand molds that breathe unevenly—determine whether a component will pass a pressure test or fail after months in service.
The difference between a durable casting and a leaker rarely shows up in a dimensional report. It lives in the way molten metal collides with air at the ingate, in the permeability of the facing sand, and in the venting strategy that no drawing ever specifies. Skilled Chinese casting suppliers have learned to read these invisible signatures, adjusting pouring temperatures and mold coatings so that air escapes before the metal solidifies, not after.
That is why the best procurement teams now ask for X-ray or CT slice images alongside the usual paperwork. The hidden airflow inside a casting is not a single defect; it is a fingerprint of the entire process. And in the competitive landscape of Chinese manufacturing, the foundries that control this invisible variable are the ones quietly winning long-term contracts.
Port Work That Shows on the Flow Bench
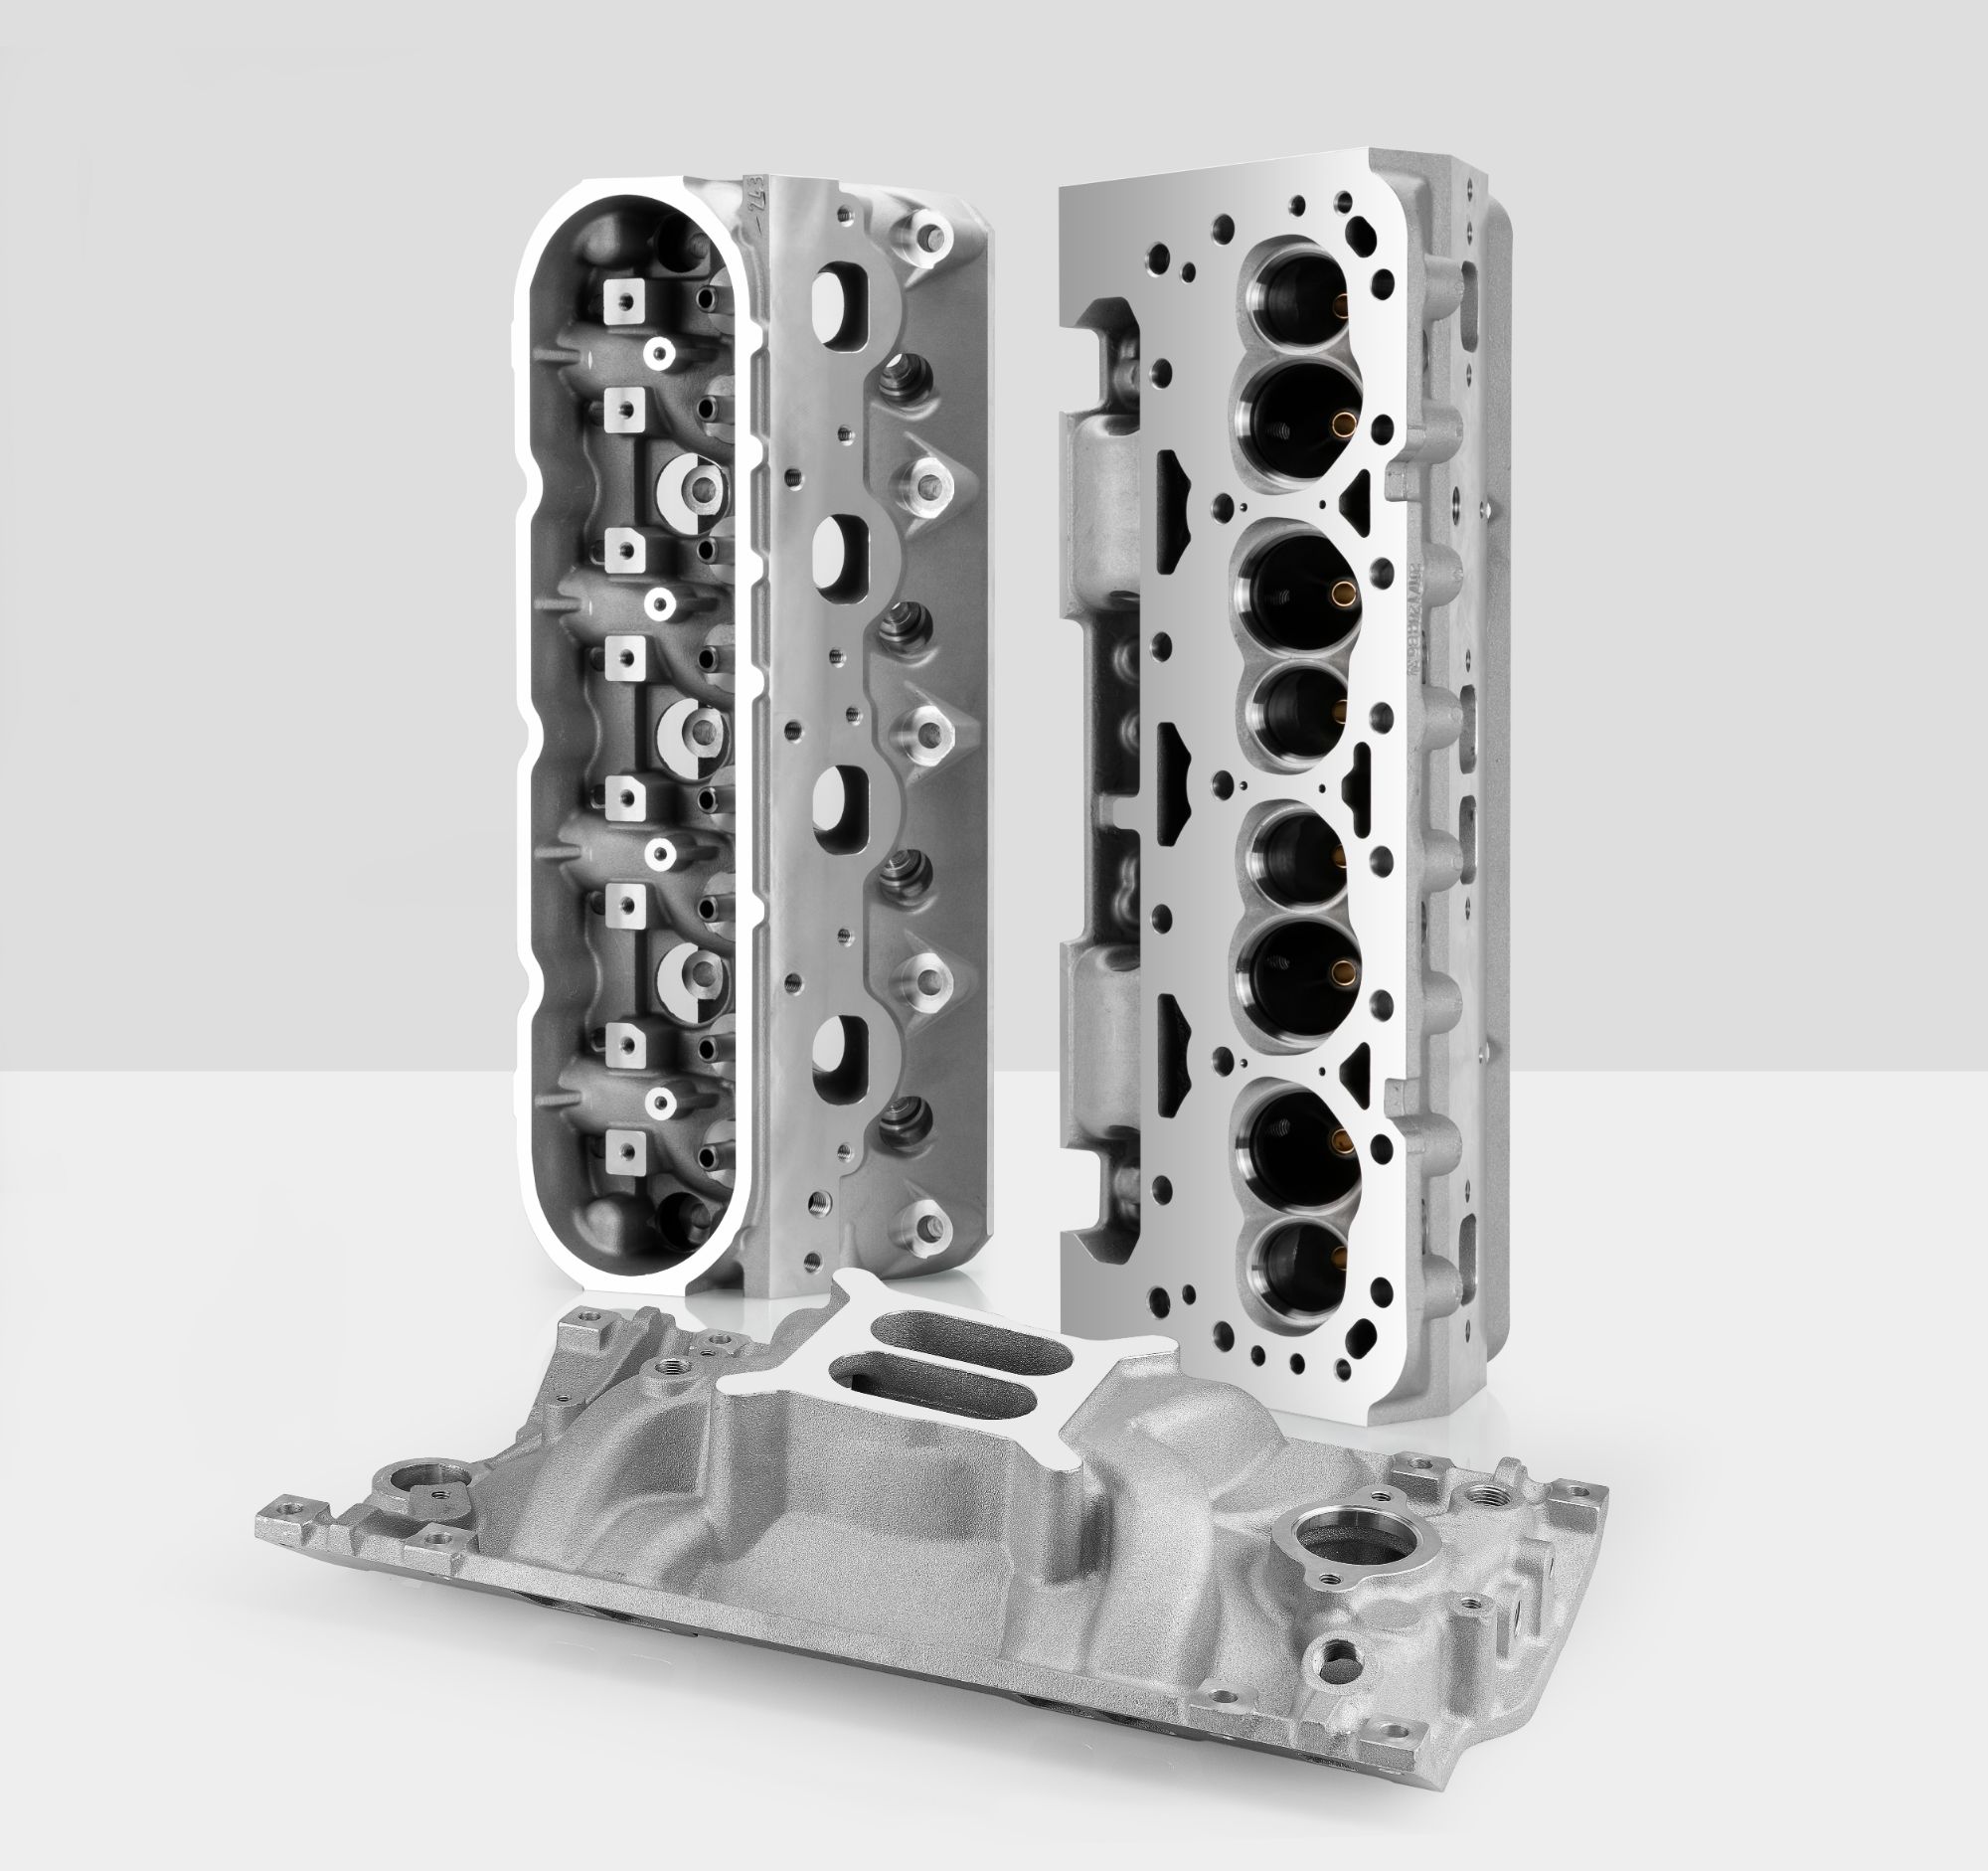
You can spend hours grinding and polishing a set of cylinder head ports, but if the numbers on the flow bench don't move, you've basically made expensive metal dust. Real port work shows up as a measurable gain in cfm, especially in the mid-lift range where the valve spends most of its time. A good hand-finish should smooth out the short-side radius and blend the bowl area without hogging out the cross-section. When you see the same head pick up 15 to 20 cfm at .400 lift, that's not luck—that's knowing where the air wants to go.
The flow bench doesn't lie, and it also doesn't care how shiny the port looks. Some of the ugliest ports with visible cutter marks outflow a mirror-polished runner because velocity and shape matter more than surface finish. A common mistake is over-polishing the intake port and killing the boundary layer, which actually hurts fuel atomization. On the exhaust side, a smooth finish helps reduce carbon buildup, but the real gains come from unshrouding the valve and straightening the roof. Watch the manometer at low valve lifts—that's where a bad seat angle or an abrupt transition will show up as turbulence, not just a lower peak number.
If you're serious about port work, log your baseline before touching anything and test after each major step: valve job, bowl blend, short-turn work, and chamber deshrouding. Small changes can stack up, but chasing peak flow at max lift often sacrifices mid-range, and that's exactly where a street engine lives. A well-ported head should show a broad, consistent gain across the curve, not just a hero number at .600 lift. When you can back up your grinding with a printout that shows more air at every lift point from .100 to .500, that's port work that actually pays off on the road.
Valve Sizing Without the Low-Lift Penalty
Many control valves are selected with a conservative margin, leading to a valve that operates mostly in the low-lift region. In this zone, the plug is still close to the seat, causing unstable flow, poor turndown, and excessive wear from high-velocity jets. The result is a loop that hunts or struggles to hold setpoint, often mistaken for controller tuning issues.
Sizing without this penalty starts with calculating the required Cv across the full range of operating conditions, not just the maximum flow. The goal is to place normal flow between 30% and 70% of valve travel, where most globe and rotary valves exhibit predictable, repeatable characteristics. If the calculated Cv keeps pulling you toward a valve that runs below 20% open, it is time to challenge the design assumptions rather than accept the oversized valve.
There are several practical fixes. Use an equal-percentage trim to get finer control at lower openings without giving up capacity. Split the duty across two valves—a small valve for startup and low-flow trim, and a larger valve for full production—so each operates in its sweet spot. Or select a valve with a replaceable reduced-capacity trim, which lets you start smaller and open up later if the process truly demands more flow. The key is to force the valve to work where it is happy, not to hope a positioner will rescue a badly sized valve.
Chamber Softening for Pump-Gas Survival
A pump's chamber doesn't fail all at once—it erodes in quiet stages, each cycle of gas pressure carving micro-channels into the metal until the once-smooth bore becomes a landscape of pitting and stress fractures. Softening the chamber before this degradation sets in isn't a luxury; it's the difference between a pump that holds its tolerance for years and one that bleeds efficiency after a few thousand strokes.
The process works by deliberately introducing a controlled plastic deformation into the chamber walls, redistributing residual stresses left from machining. This pre-compression acts like a shock absorber, letting the surface yield microscopically under gas pulsation instead of cracking. Operators often notice the change first as a drop in vibration harmonics—less high-frequency chatter, more of a low, steady thrum that suggests the material is finally breathing with the pressure instead of fighting it.
Field data from sour-gas installations shows that chambers softened this way can outlast conventional hardening treatments by a factor of two or three, particularly when the gas carries abrasive fines. The real trick isn't just surviving the first blowout; it's ensuring that after five years of cyclic loading, the chamber still has enough ductility left to absorb the next pressure spike without turning brittle.
Surface Prep That Keeps Head Gaskets Seated
Most head gasket failures blamed on the gasket itself actually start with a deck that isn't clean or flat. Before you even open the new gasket package, run a straightedge across the block and head in six directions: lengthwise, widthwise, and both diagonals. A feeler gauge will tell you if the surface has warped beyond spec—anything over about 0.002 in. across a typical four-cylinder deck needs machining, not just a thicker gasket.
Once flatness checks out, remove every trace of the old gasket with a plastic scraper or a razor blade held at a low angle. Avoid abrasive discs or rotary scuff pads on aluminum surfaces; they can leave low spots or embed grit that holds the new gasket away from the metal. Wipe the deck with a lint-free cloth and a fast-evaporating solvent until it comes back clean. If the cloth shows any gray or black, keep wiping.
A properly prepped surface should feel smooth but not polished. Many MLS gaskets want a surface finish in the 30–60 Ra range, which gives the embossed sealing beads enough tooth to bite without allowing leaks. Check the head bolt holes too—leftover oil or coolant can hydraulic-lock a bolt and create false torque readings. Chase the threads and blow them dry before final assembly.
Matching the Cam to the New Flow Curve
A cam ground for the old head often falls flat once the port work changes the bench numbers. If the new curve shows big gains between .100 and .300 inch lift but barely moves at peak, the old lobe may be leaving power on the table. You can’t just drop in the same specs and expect the engine to respond. The valve events need to spend more time in that improved lift range, which usually means revisiting duration at .050, ramp rate, and even rocker ratio.
Compare the new flow curve against the cam’s actual valve lift profile. Mark the lift points where the head now flows significantly better—say, where the discharge coefficient jumps by 5 percent or more. Then look at how many crank degrees the valve stays in that zone. If the cam barely dwells in the newly efficient window, either add lift or stretch the duration where it counts. A cam with a slower ramp may have made sense with the old head because airflow stagnated early. Now that the port keeps pulling to higher lift, a steeper ramp and more peak lift can turn extra airflow into cylinder fill.
One pitfall is ignoring low-lift flow changes. When the new curve picks up below .200 inch lift, the same overlap period becomes more sensitive. You might need to widen the lobe separation angle or trim exhaust duration to avoid reversion at part throttle. The only reliable way is to plot the measured flow at each 0.050-inch lift increment against your proposed valve events, then adjust until the cam spends the largest portion of the induction cycle in the lift range where the head actually moves air, not where you wish it did.
FAQ
It goes beyond a simple swap. You're looking at CNC porting, larger valves, upgraded springs and retainers, reshaped combustion chambers, and often a more aggressive cam profile. For serious builds, it's about maximizing airflow and combustion efficiency, not just bolting on a shiny part.
Modern Chinese manufacturing has stepped up massively. Many facilities now use the same CNC machines and quality-control processes as Western shops, but with lower overhead. That means you can get a fully ported head with oversized valves for a fraction of the price—provided you buy from a reputable supplier that shares flow bench data.
It depends on the head's specific design. Some are tuned for low-end torque and driveability, while others target high-RPM horsepower. You need to match the head to your cam, intake, and intended use. A good supplier will tell you the operating range rather than just selling you the most aggressive option.
On a stock engine, a well-designed performance head might add 15-25 horsepower. On a built engine with higher compression and a bigger cam, gains of 40-60 horsepower aren't uncommon. But numbers vary widely by engine family, so treat any exact claims with skepticism and look for before/after dyno sheets.
Start by defining your RPM range, compression ratio, and airflow needs. Check the head's intake runner volume and valve sizes against your engine's displacement. If the supplier can provide flow bench figures at multiple lift points, that's a good sign. Avoid heads that are advertised as 'one size fits all'.
It's manageable for a competent home mechanic with a torque wrench and some patience. The critical steps are proper head gasket selection, head bolt torque sequence, and checking valve-to-piston clearance if you're running a bigger cam. If you're unsure, a machine shop can assemble the valves and springs for you.
Most performance heads use aluminum castings for weight savings and better heat dissipation. Porting is usually CNC-machined to a specific shape, then hand-finished in the bowl area. Valves are often stainless steel or titanium, and springs are upgraded to handle higher lift and RPM.
The gap has narrowed considerably. If the casting is dense and the machining tolerances are tight, a Chinese-made head can last just as long as a name-brand unit. The key is to inspect the head on arrival—check valve seat concentricity, spring pressures, and deck flatness. A quality supplier will stand behind their product with a warranty.
Conclusion
When a serious engine build starts with a Chinese cylinder head casting, the first thing worth scrutinizing is what the factory left inside the ports. Core shift and inconsistent as-cast surfaces often hide usable airflow that only shows up once you map the runner cross-sections and blend the bowl area into the seat. A good porting session on these heads isn't about hogging out material—it's about evening up the short-side radius and getting the throat percentage right so the flow bench numbers climb without turning the port lazy. That same bench data also guides valve sizing. Going too big on the intake valve can kill low-lift flow, making the engine soggy off the corner when the cam comes back on. The trick is finding the diameter that works with the existing port shape, not against it.
Beyond port and valve work, the combustion chamber needs attention if the engine will live on pump gas. Sharp edges around the plug boss and the valve seats are hot spots that invite detonation, so a light chamber softening goes a long way toward making real compression survivable on 91 or 93 octane. While you're there, surface prep matters more than most builders admit. A deck that's too smooth or too coarse will fight the head gasket, especially once boost or nitrous is in the picture. The right finish helps the gasket bite and stay put. Finally, once the head flow curve changes, the old camshaft becomes a mismatch. Re-grinding or selecting a new stick around the measured mid-lift and high-lift gains brings the whole package together, letting the upgraded head actually deliver the power it promised on the bench.
Contact Us
Contact Person: Shelly
Email: [email protected]
Tel/WhatsApp: 8613967667688
Website: https://www.yongyu.com/