China Coupling Sleeve Factory for High-Performance Industrial Couplings
2026-09-14
Behind every smooth-running drive system is a component that rarely gets the credit: the coupling sleeve. At PULANKA’s China coupling sleeve factory, these precision-machined parts are built to handle the punishing loads, misalignment, and vibration that high-performance industrial couplings face every day. If you’ve ever wondered what separates a coupling that lasts a decade from one that fails in months, the answer often starts here.
Why Sleeve Hardness Specs Rarely Tell the Whole Story
Most sleeve hardness ratings come down to a single Shore durometer number, but that figure only measures the material's resistance to indentation under a specific probe. It says nothing about how the sleeve feels when it's actually installed, how it rebounds after being pinched, or whether it hardens noticeably in cold weather. Two sleeves with identical durometer readings can feel completely different in your hand because thickness, inner lining, and even the curvature of the tube change the perceived stiffness.
Lab tests for hardness are typically run on flat, thick samples at room temperature with a slow, steady press. Real-world use rarely looks like that. A sleeve on a hydraulic cylinder, for instance, gets squeezed rapidly, heated by friction, and exposed to oils or UV light. Those conditions can soften some compounds and stiffen others, making the printed spec a poor guide to long-term behavior.
What often matters more is resilience—how quickly the material springs back after deformation—and hysteresis, or the energy lost during repeated flexing. A sleeve that tests softer on paper might actually provide better support because it recovers faster, while a harder-spec sleeve can feel dead and transmit more vibration. Hardness alone is just the opening line, not the whole conversation.
Tolerance Stack-Ups That Make or Break a Coupling
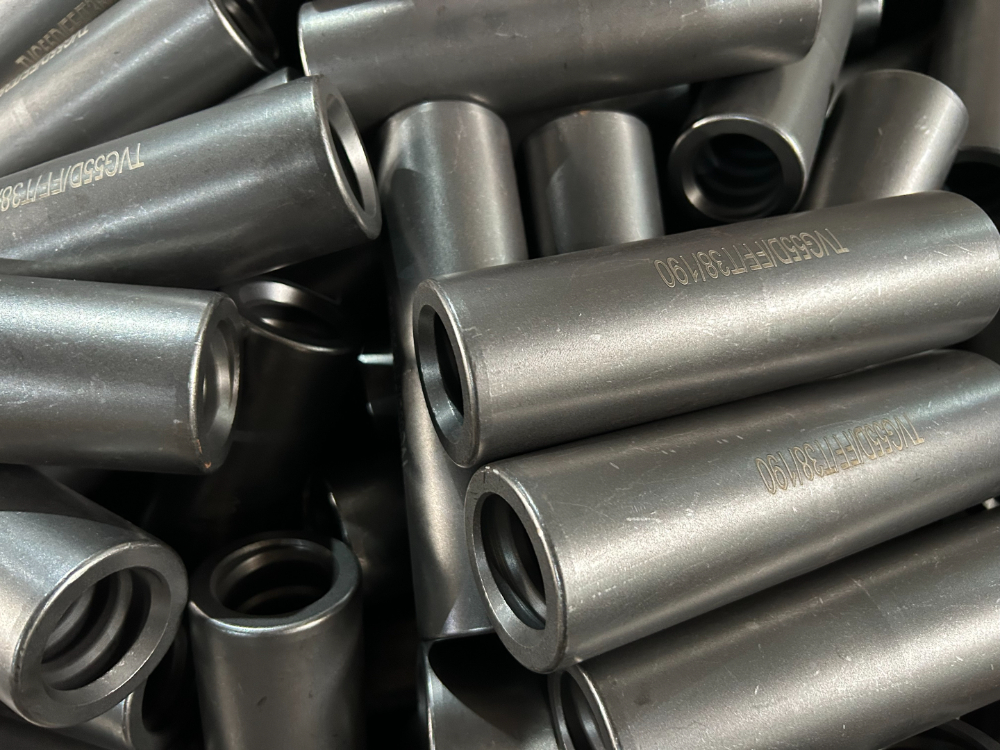
Most coupling failures blamed on poor alignment actually start long before the dial indicator ever touches the hub. A bore diameter near its upper limit, a shaft journal near its lower limit, and a keyseat with a fraction of a degree of asymmetry may each pass incoming inspection without comment. Stack them together, though, and the hub seats slightly off-center, the key cocks under load, and the resulting runout shows up as vibration nobody can trace to a single bad dimension. That is why the real question is not whether each feature meets print, but how the individual deviations accumulate in the worst-case or statistical sense.
Axial and angular buildup tends to be even more unforgiving. The gap between shaft ends, the coupling’s own length tolerance, motor magnetic center offset, and thermal growth can all push in the same direction, stretching or crushing an elastomeric element beyond its designed flex range. On the angular side, a few thousandths of an inch in bearing pedestal height combined with baseplate flatness error and hub face runout can easily exceed the manufacturer’s maximum misalignment allowance. Field experience shows these failures are rarely the result of a single out-of-spec part; they come from treating each tolerance as an island instead of running a full stack-up at the design stage.
A Walk Through Our Raw Bar Stock Inspection
Every inspection starts with the ice. Not just any ice, but the crushed, salted blend that keeps oysters, clams, and shrimp at a steady 34°F. We run our hands through the top layer, checking for meltwater pooling or uneven chill. A warm pocket near the back corner of the drawer is a warning sign, so we rotate the trays before a single shell gets tapped for service.
Next comes the tag check. Each bag of bivalves carries its harvest date and location, and we verify that every batch falls within our holding window. If a tag is missing or smudged, that product is set aside immediately. We don't guess with shellfish. The shells themselves tell a story too—tightly closed, heavy with liquid, and free of cracks. A light tap on an open shell should make it snap shut. Ones that don't respond get discarded, no second thoughts.
Finally, we log the findings in a small notebook kept by the raw bar. It isn't digital, and that's deliberate. The handwritten notes force us to slow down and notice patterns—temperature drift on busy weekends, a supplier's inconsistent sizing, a batch of clams that opened slower than usual. By the end of the walk, every tray is repositioned, every questionable piece is gone, and the raw bar is ready to shuck clean.
Surface Finishes That Delay Fretting in Wet Conditions
Moisture complicates fretting by acting as both a lubricant and a corrosion promoter, often accelerating crack initiation at the contact edges. One practical countermeasure is a manganese phosphate conversion coating, which builds a porous crystalline layer on steel. Those pores hold oil or dry-film lubricants even under repeated water washing, so the interface keeps a low shear resistance instead of turning into a stick-slip zone. The result is a noticeable delay in the transition from mild polishing to severe surface disruption.
Shot peening and laser shock peening take a different route: they leave behind compressive residual stresses that blunt microcrack tips before they can grow into fretting fatigue failures. In wet or condensing environments, these treated surfaces also shed corrosion debris more easily, since the hardened near-surface layer resists the formation of water-softened oxide agglomerates. Combined with a thin diamond-like carbon coating, the hydrophobic nature of the film discourages water from wicking into the contact and keeps the debris layer dry and less abrasive.
Anodizing or micro-arc oxidation on aluminum alloys creates a thick ceramic layer with micron-scale pores that can be sealed with hydrophobic agents or solid lubricants. In humid service, capillary action normally pulls water into tight clearances and accelerates fretting corrosion, but a properly sealed anodic layer flips that behavior. The sealed pores hold lubricant in place, while the surface tension of water droplets prevents them from spreading across the wear scar. This keeps the contact region starved of free water, so the fretting damage progresses at a much slower rate.
When Off-the-Shelf Sleeves Are Not an Option
Standard protective sleeves assume a world of uniform cables, predictable connector sizes, and gentle handling. Reality rarely cooperates. Custom terminations, oversized plugs, awkward Y-splits, or tight routing through machinery quickly defeat generic off-the-shelf options. Instead of forcing your assembly into a sleeve that fights back, you end up with bunching, exposed sections, or painful installation workarounds.
Tailored sleeving addresses these pain points directly. By matching the sleeve's diameter, stretch, and end finish to your actual harness geometry, you get full coverage without excessive bulk. Odd shapes, breakouts, and strain-relief points can be accommodated seamlessly. The result is a protective layer that fits like a second skin, not a borrowed coat.
Choosing a custom solution also opens the door to specialized materials and coatings that stock sleeves simply don't offer. Whether you need extreme temperature resistance, chemical tolerance, or a specific durometer for abrasion, the sleeve can be engineered around your environmental demands. Off-the-shelf might be fine for prototypes, but when reliability and a clean install matter, a made-to-measure approach pays for itself.
Balancing Throughput and Metallurgy in a Chinese Plant
At the heart of the plant's daily operation lies a tension that no amount of scheduling software can fully resolve: pushing more tons through the mill almost always tugs against the delicate chemistry of the steel itself. The operators know that a faster rolling speed can shave minutes off each coil, but it also raises the risk of finishing temperatures drifting out of the narrow band needed for the target grain structure. In practice, the shift supervisor often stands between the pulpit and the cooling banks, watching the pyrometer readings and making small, almost instinctive adjustments to the water flow or the line speed. These tweaks are rarely written down; they live in the collective memory of the crew, passed from one shift to the next like a dialect.
Metallurgy, for its part, refuses to be rushed. The transformation from austenite to ferrite, the precipitation of carbides, the bite of the last pass on the hot strip mill—each step has its own clock, and ignoring it costs more than a few downgraded coils. A batch of high-strength low-alloy steel that cooled too quickly might pass the tensile test in the lab but fail later in a customer's stamping die. So the plant has learned to build slack into the supposedly lean schedule: not idle time, but deliberate pauses that let the material catch up with the process. One furnace operator described it as "letting the steel breathe between squeezes," a phrase that never appears in any standard operating procedure yet captures the rhythm better than any KPI.
The real balancing act happens at the interface between the caster and the hot strip mill, where a surge in throughput upstream can flood the reheat furnace and force the mill to run at a pace that punishes the metallurgy. To cope, the plant has quietly abandoned the idea of a fixed target for tons per hour. Instead, the production team resets the target at the start of each campaign, based on the grade mix, the expected slab temperatures, and even the ambient humidity that affects cooling rates on the run-out table. This is not a compromise but a recognition that throughput and metallurgy are not enemies; they are two dialects of the same language, and the plant's fluency comes from knowing when each should speak.
FAQ
We primarily work with carbon steel, stainless steel, aluminum alloys, and engineering-grade plastics. Material selection depends on torque requirements, operating environment, and corrosion concerns. For demanding applications, we also offer heat-treated alloy steel options.
Yes, custom work is a significant part of our production. Customers can supply drawings or samples, and our engineering team will review tolerances, keyways, and hub dimensions. We handle both small prototype runs and large volume orders.
Every batch undergoes dimensional inspection, material certification checks, and dynamic balancing when required. We also perform hardness testing and keyway profile verification before shipping. This process helps catch potential issues early and keeps failure rates very low.
Our components are used in steel mills, paper processing, mining conveyors, power generation, marine propulsion, and automated manufacturing lines. The common thread is a need for torque transmission that can handle vibration, misalignment, and continuous operation.
We offer phosphating, black oxide, zinc plating, Dacromet coating, and epoxy painting. The choice depends on exposure conditions, such as humidity, chemicals, or saltwater. We can recommend a treatment based on the working environment.
Standard sizes with common bore dimensions can often ship within 7 to 14 days if materials are in stock. Custom designs usually take 4 to 7 weeks, depending on machining complexity, heat treatment requirements, and current production load.
Yes, we machine sleeves to match specific coupling series from major manufacturers as well as proprietary designs. We need the coupling type, bore size, keyway dimensions, and sometimes a sample or drawing to ensure proper fit.
We keep a buffer stock of common sleeve sizes and can prioritize rush jobs when equipment is down. Our production team can add overtime or split batches across machines to shorten lead times. Communication is key, so we ask customers to share the urgency level as early as possible.
Conclusion
Hardness specs rarely tell the whole story. A coupling sleeve that passes Rockwell testing can still fail early because the real drivers are case depth, carbide morphology, and how the hardness transitions near the keyway. In our plant, incoming bar stock gets spectrographic verification and a macroetch check before it ever reaches a lathe. That front-end step prevents hidden segregation from becoming a tolerance nightmare later, especially when bore, keyway, and OD dimensions stack up against each other.
Surface finish plays a bigger role in wet conditions than most designers admit. A finish that is too polished can starve the interface of lubricant, while a rough one accelerates fretting; we hold a specific Ra window and verify it with profilometry at the grinding station. When standard sleeves are not an option, we move to custom turning and induction hardening with in-house metallography to confirm the case pattern. Balancing throughput with metallurgy in a Chinese factory is not about cutting corners—it is about batch-level process control, furnace log reviews, and daily hardness audits that keep lead times short without turning heat treatment into a black box.
Contact Us
Contact Person: Elma
Email: [email protected]
Tel/WhatsApp: +86 13738628777
Website: https://www.pulankagroup.com/