Best Sliding DU Bushing Options for Smooth and Durable Motion
2026-11-16
Sliding DU bushings are everywhere, but 'everywhere' doesn't mean equal. Some seize, some squeak, and some quietly eat away at your maintenance budget. If you're tired of replacing bushings long before they should fail, you're in the right place. Below, we compare the best DU bushing options for genuinely smooth, durable motion—including a closer look at why XIAYI consistently earns a spot in demanding applications.
Why DU Bushings Run Smoother Than Standard Bronze Sleeves
Standard bronze sleeves depend on a continuous film of grease or oil to separate the shaft from the bearing. When that film thins out, gets squeezed away under load, or collects dirt, you get metal-to-metal contact that feels like grabbing, stick-slip, or a rough start. DU bushings get rid of that dependency. They have a thin PTFE-based liner bonded over a bronze backing, so the sliding surface lubricates itself from the very first movement. The friction stays low and steady even during slow oscillating motion or frequent starts and stops where plain bronze tends to bind.
Another reason DU runs smoother is how it handles wear particles. In a standard bronze sleeve, tiny bits of grit or metal debris can become trapped at the contact surface and score the shaft, which shows up as vibration and uneven travel. The softer PTFE liner in a DU bushing allows those particles to embed and get covered, keeping the shaft on a cleaner, more uniform film. Over time that reduces micro-wear and lets the motion stay fluid cycle after cycle instead of getting progressively rougher.
Clearance also plays a role. Bronze sleeves usually need extra space for a lubricant film and thermal expansion, and that gap can introduce slight play or rattle as the shaft reverses direction. DU bushings are typically press-fit and conform to the housing, so they damp small misalignments without the clearance-related slop. The result is a tighter feel, less audible noise, and a smoother stroke from the first cycle onward.
The PTFE Layer Does the Heavy Lifting Without Grease
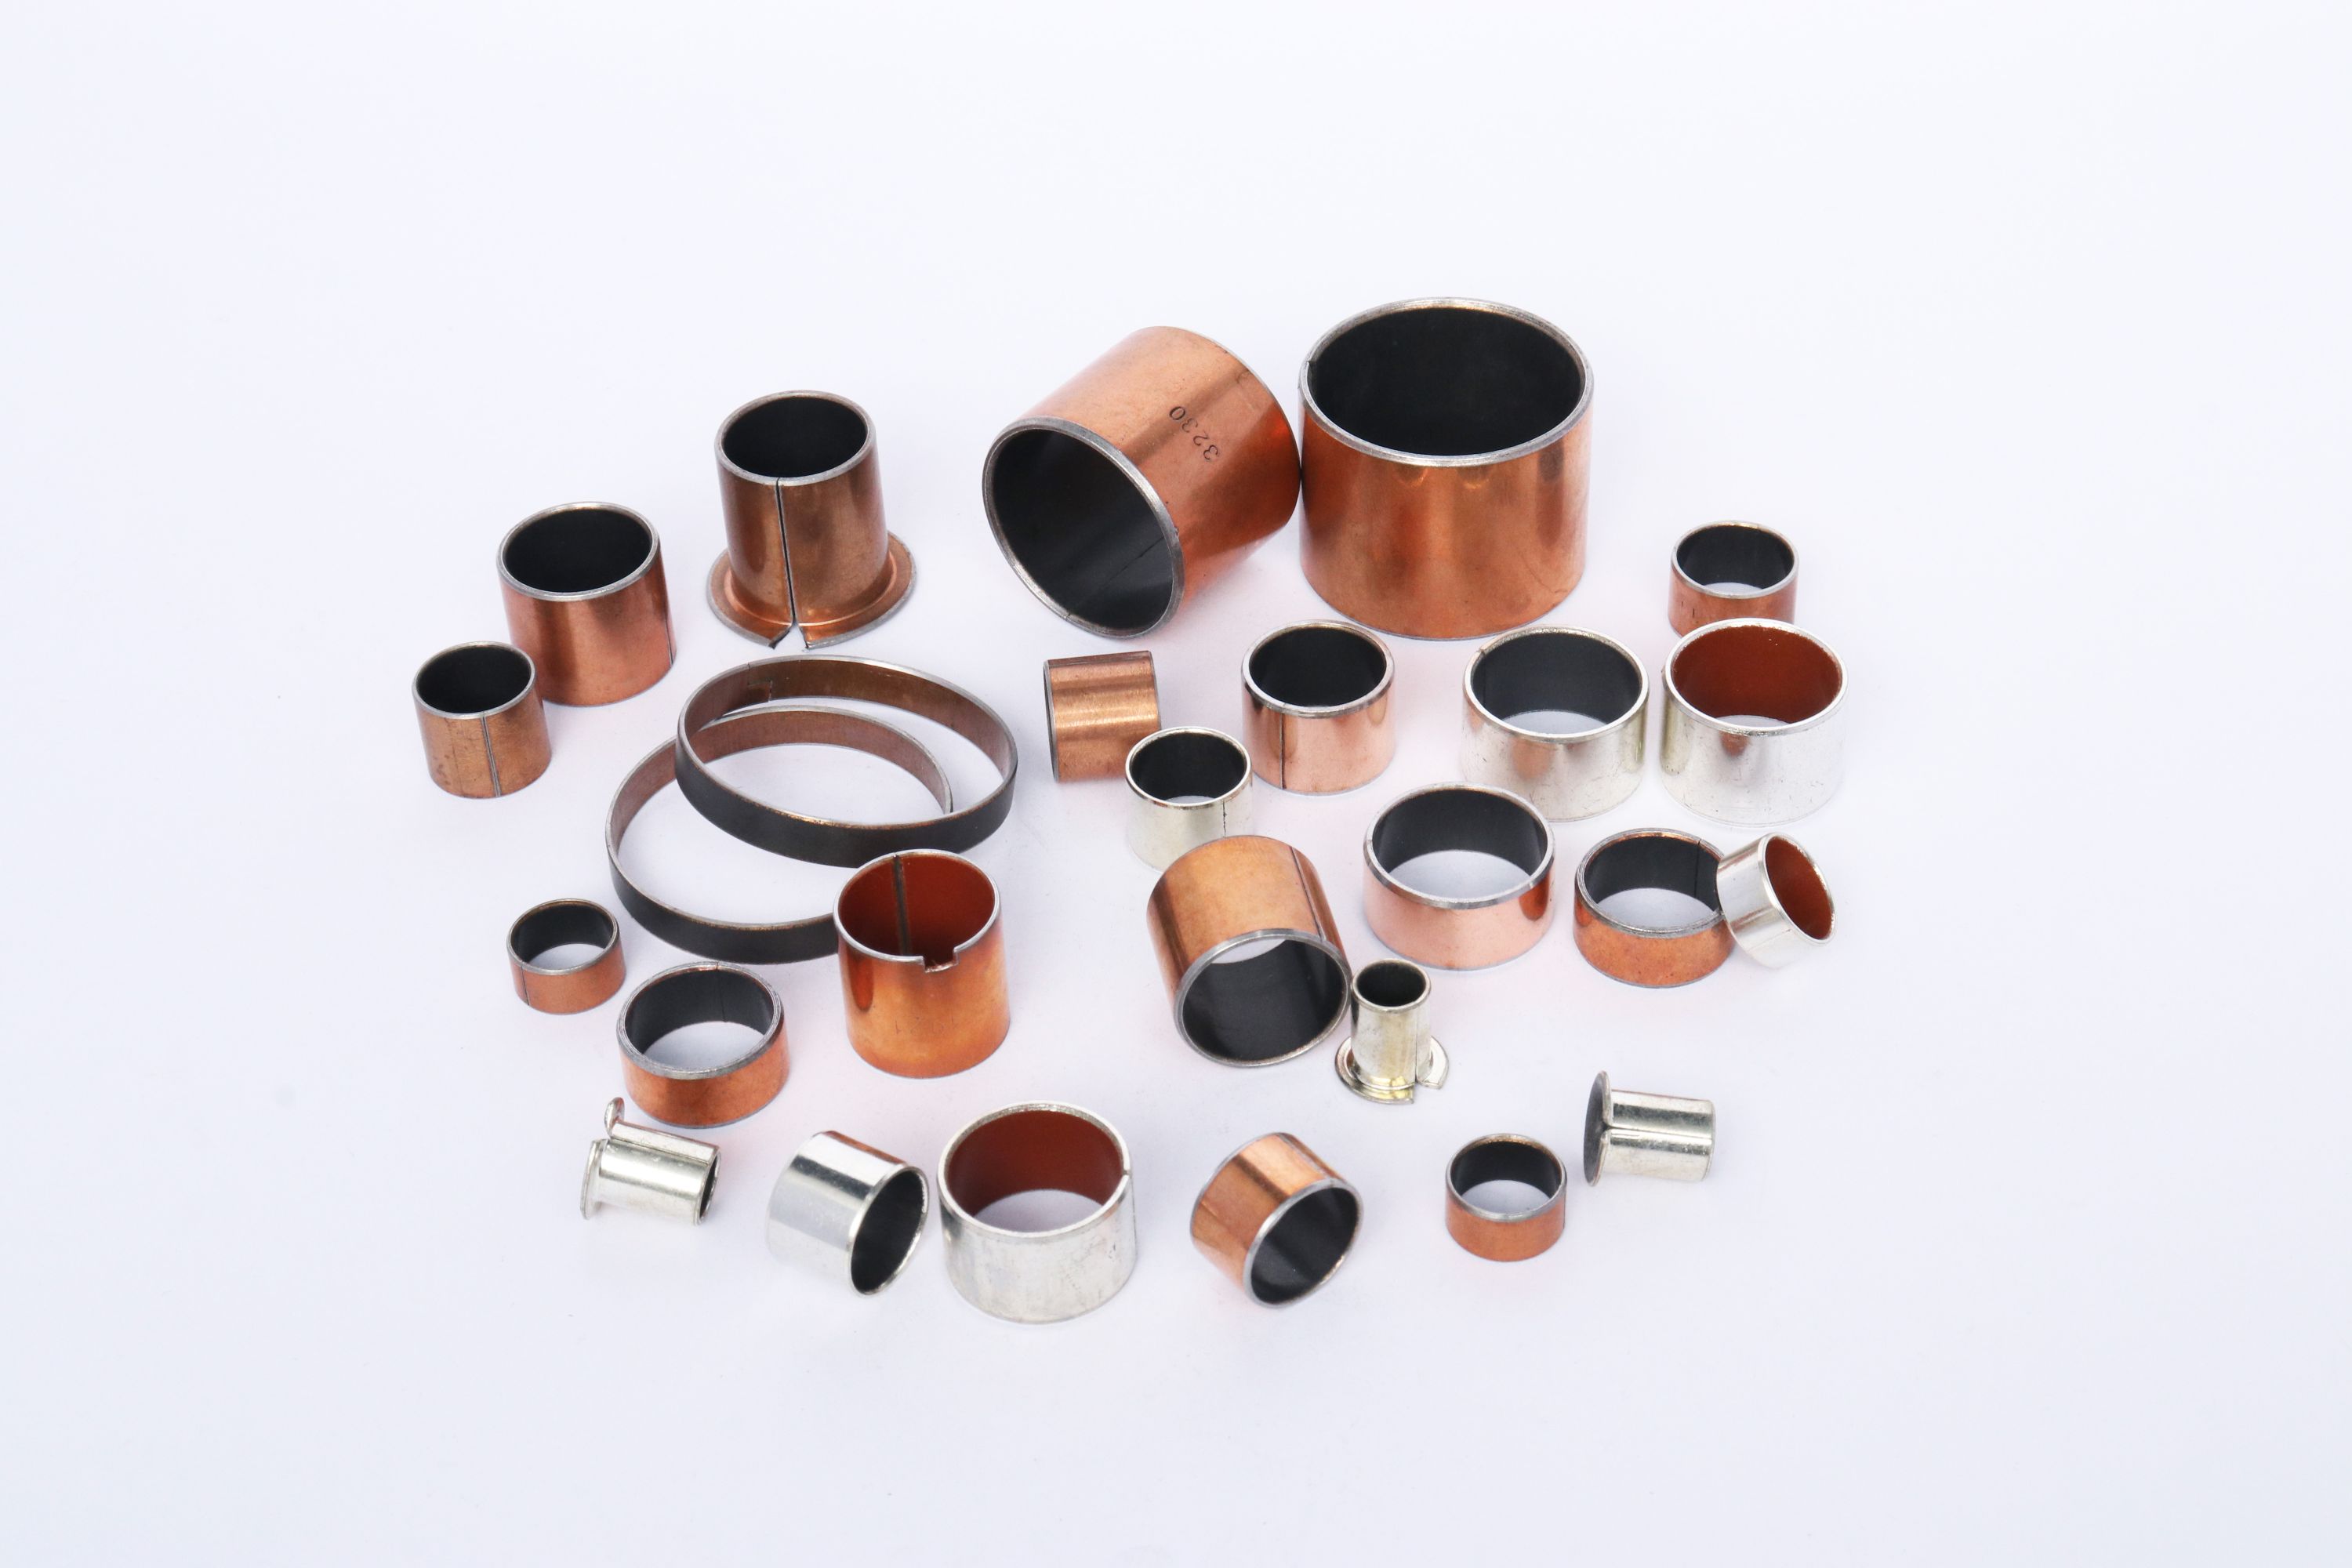
Most non-stick surfaces only work if you add a slick of oil first. Not here. The PTFE layer takes over from the moment food hits the pan, letting eggs slide, cheese crisp, and delicate fish lift off without tearing. You can skip the butter or spray entirely and still watch food release with a gentle nudge.
That means less smoke in the kitchen, fewer added calories, and a quick rinse under the tap instead of a soaking session. Over time, the surface stays reliably slick because it doesn't rely on a grease build-up to perform. The heavy lifting? Done silently, every single cook.
Load Ratings, Speed Limits, and the Numbers That Actually Matter
Most drivers glance at the sidewall and see a wall of numbers, but only a few actually change how the tire behaves on the road. Load rating and speed symbol are the pair that determine whether a tire can safely carry your vehicle at highway pace, not the marketing claims about ultra-high performance or all-season grip. If you ignore these two, you can end up with a tire that looks right on paper but overheats or flexes too much under real weight.
Load index is not a weight limit in pounds written directly—it’s a code that maps to a specific kilogram figure per tire. A rating of 91, for instance, means 615 kg per tire, and you need all four working together to cover your axle loads. Going lower than the vehicle manufacturer’s spec might save a few dollars, but it reduces the safety margin for hard cornering, heavy braking, and pothole impacts. Speed rating works differently than most assume: it’s not a green light to drive at that number, but a certification that the tire can dissipate heat at sustained high speed. An H-rated tire can handle 210 km/h in a lab, but that doesn’t make it a good idea to hold that speed on a loaded vehicle in summer traffic.
What actually matters is the combination. A high speed rating with a low load index is a trap—you get a tire that can spin fast but not carry the weight of a full cabin and luggage without overheating its internal structure. Conversely, an extra-load XL tire with a modest speed symbol often gives better real-world durability for crossovers, EVs, and family cars than a softer, faster tire that looks impressive on a spec sheet. Before buying, check the placard in the door jamb, not the maximum the tire claims, and keep the actual load per axle in mind, not just the number molded on the side.
Getting the Press Fit Right So DU Bushings Don't Move
A DU bushing that shifts under load usually points back to a press fit that was guessed at rather than measured. The housing bore needs to be round, clean, and a couple tenths undersized relative to the bushing OD, but that undersize has to be uniform. If the bore is bell-mouthed or scored, contact pressure drops in those spots and the bushing works loose after only a few hundred cycles. Take the time to check the bore in at least three places and two planes before installation.
Installation force is another giveaway. If the bushing slides in with little resistance, there is not enough interference to hold it once the shaft starts rotating. A proper press fit should require steady, controlled force from an arbor press or threaded tool. Hammering is a shortcut that usually ends with the bushing going in crooked, which scrapes material off one side and creates a loose spot from day one. Use a driver that contacts the full face and keep the bushing square to the bore during the entire press.
Once seated, do not rely on retaining compound to make up for a bad fit. It may fill microscopic gaps, but it will not replace missing metal or correct an oval bore. If the old bushing spun or walked out, measure the housing carefully before ordering a replacement, and consider staking or pinning only as a secondary safeguard after the press fit itself is proven. A properly sized interference fit is what keeps a DU bushing where it belongs, not glue or hope.
Quiet, Low-Maintenance Spots in Machinery That Suit DU Bushings
Some of the best places to use DU bushings are tucked away inside equipment where service access is limited and noise is unwelcome. Think of pivot joints on slow-moving conveyor rollers, linkage arms in packaging machines, or the oscillating shafts of textile looms. These spots rarely get attention until something starts squeaking or seizing. A DU bushing with its PTFE-lead lining handles light to moderate loads without needing a constant grease supply, which means fewer maintenance calls and a noticeably quieter operation compared to a dry metal-on-metal contact.
Other ideal candidates include the hinge points of agricultural spray booms, the guide rods on small linear actuators, and the pedal pivots in commercial kitchen equipment. What makes these locations special is that they often run in dusty or washdown environments where traditional grease fittings either clog or get washed out. The low-friction surface of a DU bushing tolerates occasional contaminants better and shrugs off moisture without corroding the shaft. You get a long, predictable wear life with almost zero upkeep, which frees up technicians to focus on more critical parts of the machine.
If you are retrofitting older machinery that has a history of sticky shafts or uneven wear, swapping in DU bushings at the low-speed oscillating joints can smooth out the motion without a major redesign. Pay close attention to bearing housings that are hard to reach, such as those behind belt guards or inside closed gearboxes with external levers. The self-lubricating property of DU material means you can extend lubrication intervals or eliminate them altogether in light-duty applications, cutting both noise and labor costs over the long run.
Signs a DU Bushing Is Nearing the End and Simple Replacement Steps
A DU bushing rarely fails without warning. You might notice a persistent metallic squeak that changes pitch under load, or visible scoring on the inner surface when the shaft is withdrawn. Play develops gradually: grab the shaft and try to rock it side to side. If you feel more than a hair of movement, the PTFE lining has worn past its useful thickness. In hydraulic or suspension applications, a dull knocking over bumps or during direction changes often points to a bushing that has lost its interference fit.
Replacement is straightforward if you catch the wear early. Remove the retaining circlip or end cap, then drive the old bushing out using a properly sized mandrel—never a screwdriver, which can gouge the housing bore. Clean the bore with a Scotch-Brite pad and wipe it dry. Press the new DU bushing in with a shouldered tool that contacts only the outer steel shell. If the fit is tight, chilling the bushing in a freezer for twenty minutes shrinks it enough to slide home without excessive force.
After installation, run a finger inside the bore to check for any lip or high spot at the seam. The split in a DU bushing is intentional; orient it away from the main load direction. Reassemble the shaft with a light smear of assembly grease, then cycle the joint a few times by hand. A properly seated bushing will feel snug but not bind, and the old squeak or knock should be gone immediately.
FAQ
DU bushings are self-lubricating composite plain bearings with a steel backing, porous bronze layer, and PTFE-lead overlay. They handle sliding motion well because the PTFE surface reduces friction without external grease, making them reliable in tight spaces or where maintenance is hard.
Start by measuring the shaft diameter and housing bore precisely, then check the bushing's wall thickness and length against your load and speed. The bushing should fit snugly but allow a slight interference fit in the housing, and the shaft tolerance should be h7 or f7 for smooth sliding.
Look for increased play or wobble, scoring on the shaft, uneven wear on the PTFE layer, or higher friction that causes heat buildup. Discoloration or flaking of the lining usually means the load or speed exceeded the bushing's range, or contamination got in.
They handle moderate to high loads, depending on the specific grade and size. Standard DU bushings work well up to about 140 N/mm² dynamic load, but for heavier loads you might need a thicker wall or a reinforced variant. Always check the PV limit for your speed and load combination.
Use a press or a proper installation tool with a flat face that matches the bushing's outer diameter. Press it in slowly and evenly into a clean, chamfered housing bore. Avoid hammering directly on the bushing edge, and never ream or machine the bore after installation, as that damages the PTFE surface.
They are designed to be maintenance-free, so no regular greasing is needed. However, you should keep the sliding surface free of dirt and debris, inspect for wear during scheduled shutdowns, and replace the bushing if the PTFE overlay is worn through to the bronze layer.
Standard DU bushings operate continuously up to about 130°C, but this depends on the specific resin used in the PTFE layer. For temperatures above that, look for high-temperature variants that use different fillers or a metal-backed design without polymer limitations.
Conclusion
When maintenance teams swap out standard bronze sleeves for DU-style sliding bushings, the difference shows up almost immediately in how the machine feels. Instead of the stick-slip judder that often plagues greased bronze, a DU bushing runs quiet and steady because its steel backing gives it structural stiffness while a thin, self-lubricating PTFE composite layer handles the sliding surface. That PTFE layer does the heavy lifting without needing a grease gun, which is a real advantage in spots where you can't easily reach a fitting or where stray lubricant would contaminate product. But you still have to respect the numbers: typical dynamic load ratings for a DU bushing might sit around 140 N/mm², and surface speed usually tops out near 2.5 m/s, though the exact limits depend on shaft hardness and finish. Ignore those figures and you'll shorten the bushing's life no matter how good the material is.
Even the best DU bushing won't perform if it's not pressed in correctly. The housing bore should be machined to an H7 tolerance, and the bushing needs a slight interference fit—usually around 0.05 to 0.1 mm depending on diameter—so it stays put under load. Once installed, these bushings thrive in low-maintenance, low-speed, high-load areas like hinge pins, conveyor rollers, agricultural linkage joints, and food-processing equipment where noise and grease are both unwanted. Over time, you'll know a DU bushing is nearing the end when you see exposed bronze through a worn PTFE surface, feel increased radial play, or hear a dry metallic squeak at startup. Replacement is straightforward: drive out the old bushing with a stepped mandrel, clean the housing, then press in the new one using a flat plate and arbor press—never hammer directly on the flange or you'll distort it.
Contact Us
Contact Person: Leela
Email: [email protected]
Tel/WhatsApp: 8613586885132
Website: https://www.xiayishockparts.com